bannière
Maison

chambre d'essai de choc thermique

chambre d'essai de choc thermique

  • Lab Companion|CPO & Optical Engine Thermal Cycling Test Solutions
    Sep 27, 2026
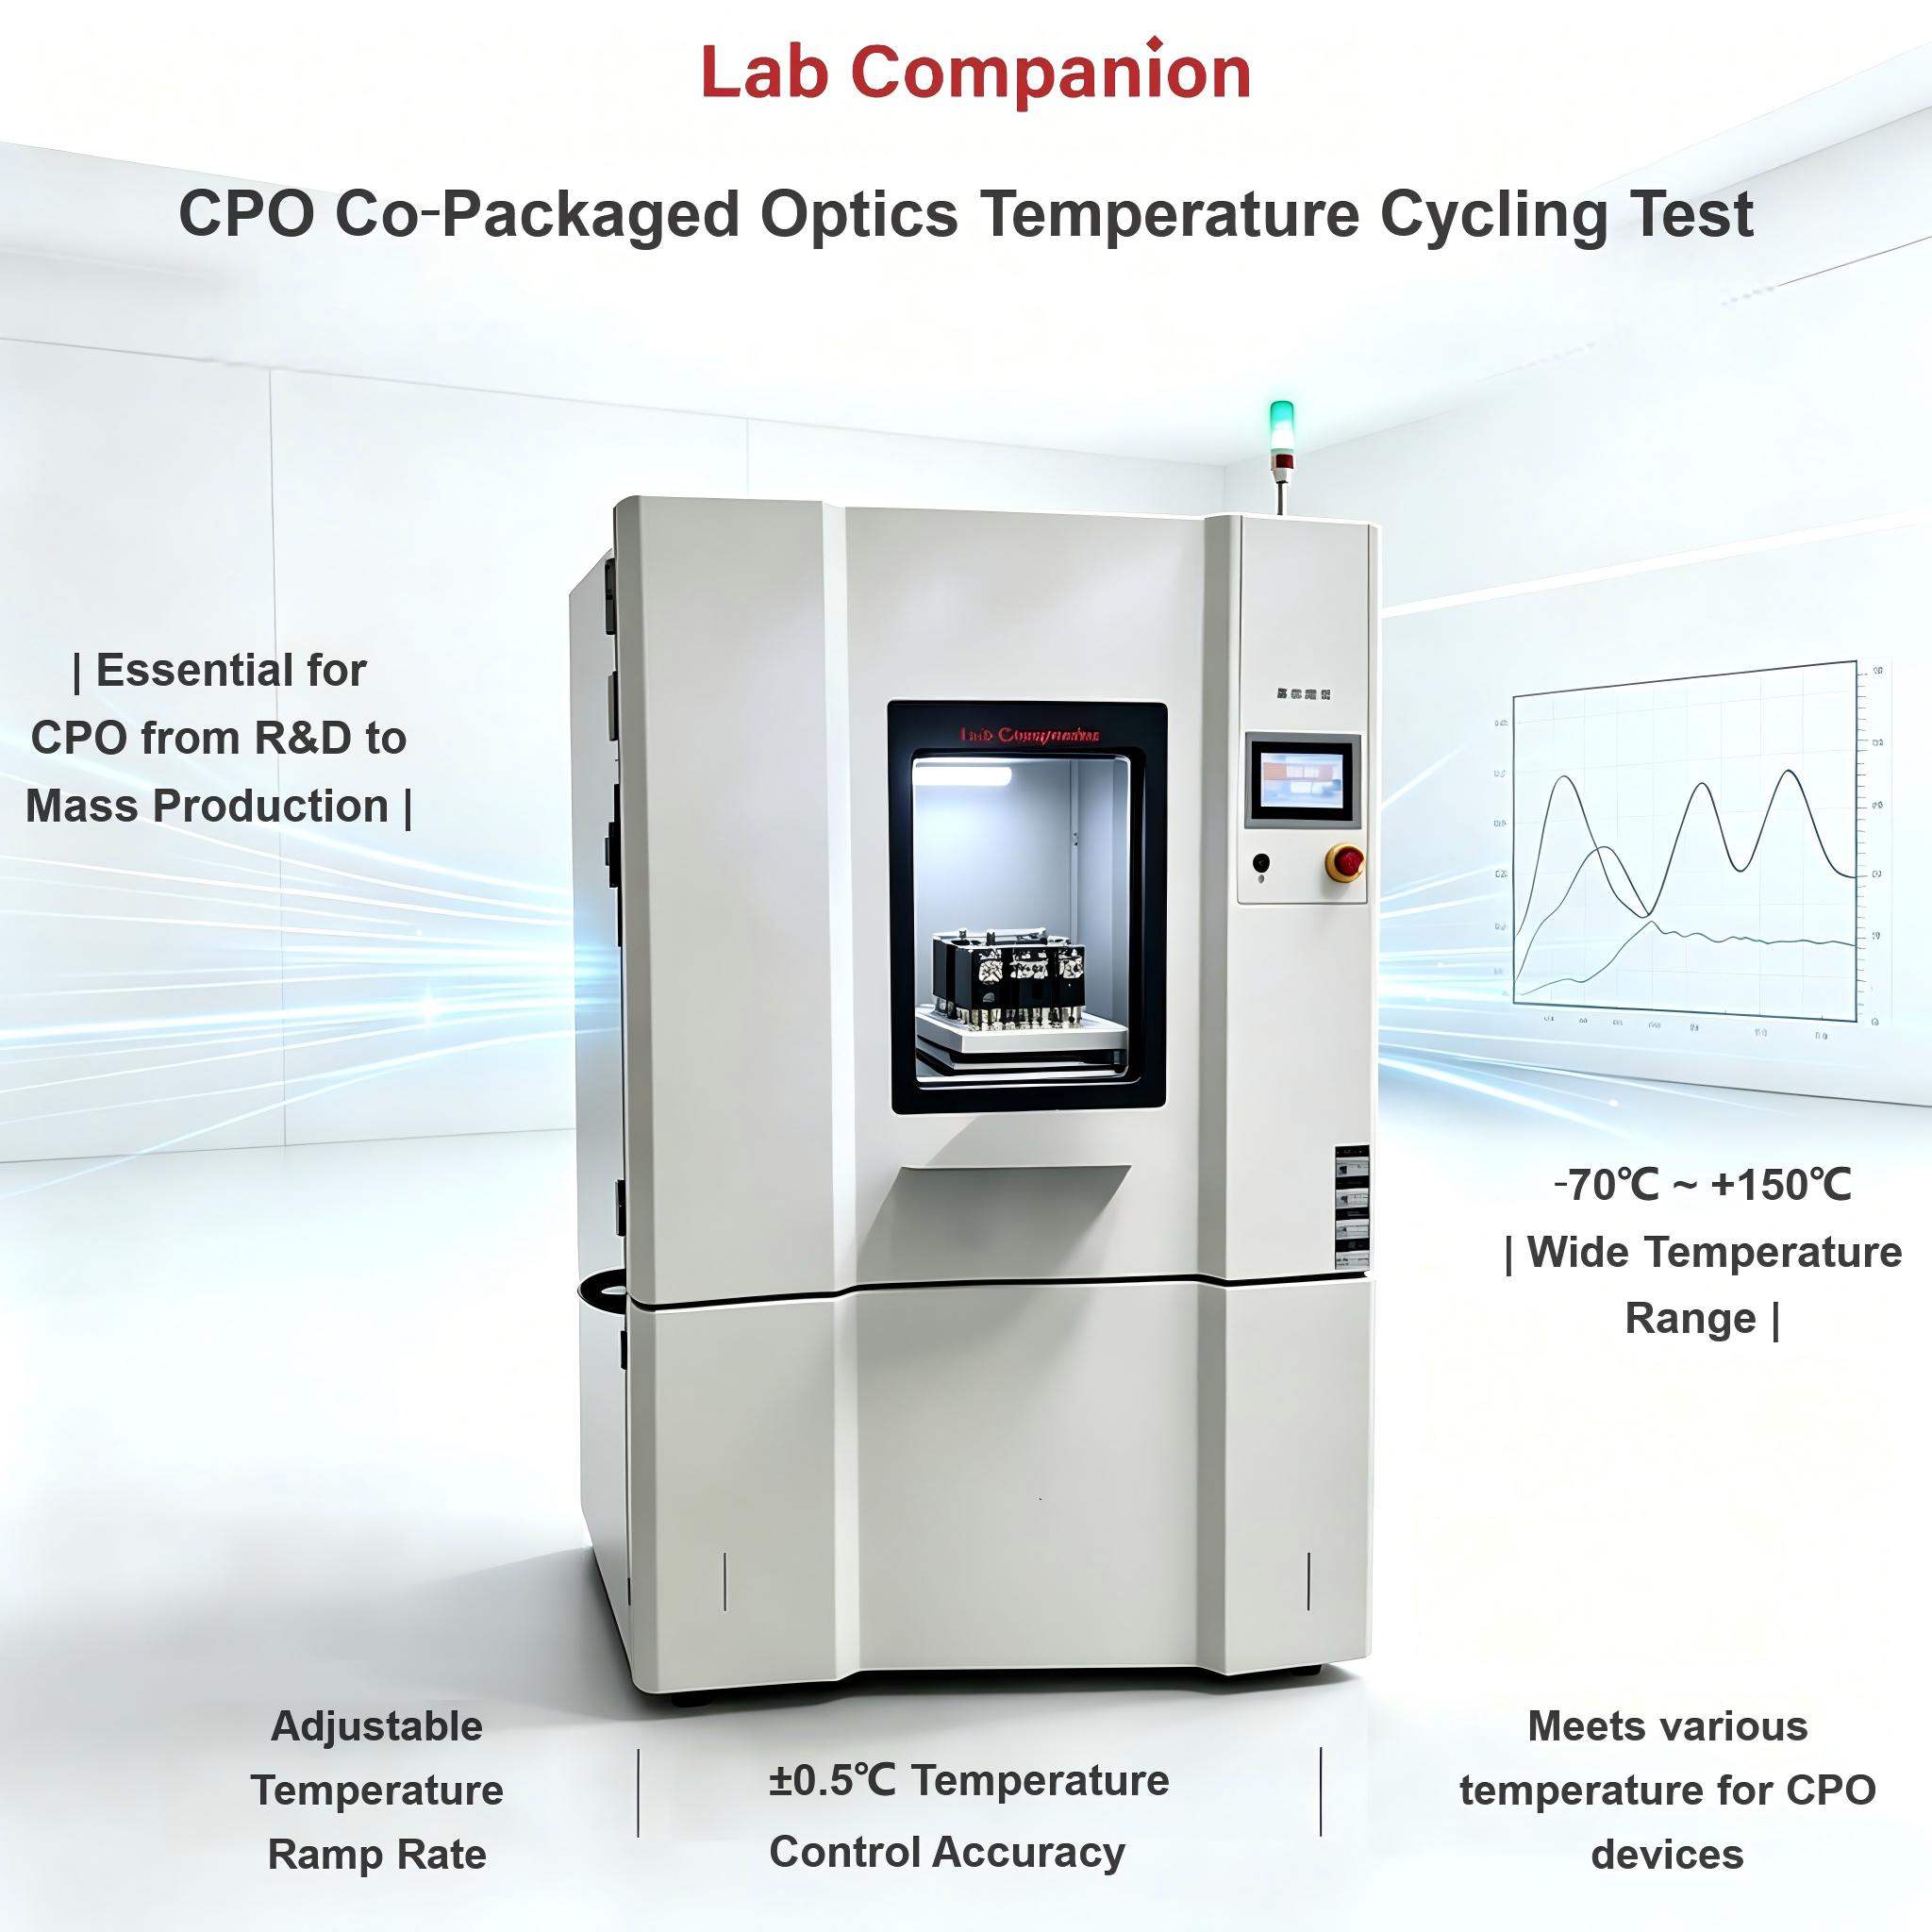
    1. CPO Industry Transition: From Lab Validation to Mass Production Driven by the rapid expansion of AI computing clusters, optical interconnection architectures are accelerating the shift from traditional pluggable optical modules to Co-packaged Optics (CPO) and Near-packaged Optics (NPO). Leading global players are scaling next-generation CPO switching platforms, while Chinese manufacturers are advancing prototype verification and mass production layout, pushing CPO from technical exhibition scenarios toward commercial deployment. By co-packaging optical engines and switch chips on a single substrate, CPO shortens optical signal transmission paths and reduces power loss. However, this highly integrated structure brings higher thermal density and more complex temperature stress distribution. At the mass-production stage, the core industry challenge is no longer technical feasibility, but high-reliability, low-cost, and large-scale manufacturability. 2. New Reliability Challenges Brought by CPO Architecture Innovation The rapid growth of large-scale GPU clusters has completely reshaped data center interconnection requirements. Traditional copper cable interconnection cannot meet the high-bandwidth, low-latency demands of AI clusters. Optical interconnection is now deployed closer to computing chips, extending from cabinet-to-cabinet transmission down to chip packaging level. Unlike conventional pluggable optical modules — which can be replaced individually after failure — CPO integrates optical and electrical chips into one sealed package. Any single device failure may lead to the replacement of the entire system. This fundamental change makes temperature cycling reliability the core indicator of CPO mass production qualification. 3. Three Core Barriers Restricting CPO Commercialization 3.1 Ultra-low insertion loss requirements for optical coupling A qualified CPO system requires optical coupling efficiency above 95% and single-joint insertion loss controlled below 0.5 dB, to maintain overall package loss within 1.8–3 dB. CPO packages multiple heterogeneous materials — including silicon photonic chips, laser chips, ceramic substrates, epoxy resin, and copper interconnects — with a thermal expansion coefficient difference of 2–8 times among materials. Repeated temperature cycling generates periodic thermo-mechanical stress, causing nanometer-level displacement of optical fibers and photonics alignment structures, which directly increases optical loss and deteriorates system performance. 3.2 Severe yield superposition risks CPO presents extreme yield superposition effects. Assuming a 95% individual optical engine assembly yield, a single switch chip integrating 32 optical engines will achieve a system-level yield of only 19%. Complex packaging and high integration significantly raise manufacturing thresholds, leading the industry to predict large-scale CPO commercialization will be delayed until 2028–2029. 3.3 Difficult post-maintenance Pluggable modules support rapid on-site replacement. In contrast, CPO’s highly integrated packaging fixes optical engines and switch chips as a whole. Once the laser or optical engine fails, the entire board needs replacement. The industry is promoting external laser source solutions to reduce maintenance costs, placing vulnerable components at replaceable panel positions. 4. Strict Temperature Cycling Reliability Standards for CPO CPO devices face far more stringent thermal reliability tests than traditional optical modules, mainly reflected in thermal failure mechanisms and optical parameter temperature sensitivity. High thermal density inside CPO packages causes thermal interface material fatigue, pump-out, and dry aging during rapid temperature cycling, continuously increasing thermal resistance. Typical failure modes include solder ball fatigue, gold wire bonding fracture, TEC delamination, substrate warpage, and fiber coupling offset — a unique failure mode of CPO devices. Optical engines are extremely temperature-sensitive. The wavelength drift coefficient of DFB lasers is 0.08–0.1 nm/°C. With mainstream DWDM channel spacing of only 0.8 nm, tiny temperature fluctuations will cause wavelength deviation, crosstalk rise, and increased bit error rate. Therefore, CPO temperature cycling tests must monitor real-time optical parameter stability rather than only structural integrity. Global industrial test standards form a complete certification matrix: • GR-468-CORE: Temperature range -40 °C to +85 °C, linear temperature rate ≥ 10 °C/min, minimum 500 cycles, 10-minute dwell time at extreme temperatures. • High-end 1.6T/ LPO upgrade criteria: Extended range of -55 °C to +125 °C, temperature rate ≥ 15 °C/min. • JEDEC JESD22-A104 & IEC 60068-2-14: Mandatory supplier qualification evaluation standards. 5. Lab Companion Full-level CPO Thermal Validation Solutions (China High-end Manufacturing) Lab Companion is a professional environmental test equipment manufacturer rooted in China, with 20+ years of R&D and manufacturing experience in reliability testing equipment. Supported by three major production bases in Dongguan, Kunshan and Chongqing, covering a plant area of over 6,000 ㎡ and an annual capacity of 1,000 sets of environmental chambers, the brand represents high-precision, cost-effective, and stable Chinese industrial manufacturing capabilities for global optical communication and semiconductor customers. Global Service Note: For overseas clients, Lab Companion provides full-process online technical guidance, remote debugging, program setting, and after-sales support. No on-site door-to-door service is available in overseas regions. Professional online support ensures consistent test accuracy and equipment operation efficiency worldwide. 5.1 Optical Engine & Module-level Solution: TC Series Rapid Temperature Change Chamber The Lab Companion TC series is specially optimized for high-density CPO optical engine screening. • Temperature range: Standard -70 °C ~ +150 °C, extended extreme test range -55 °C ~ +125 °C • Temperature rate: 5/10/15/20/25 °C/min (full loaded actual test rate, linear controllable) • High precision control: Temperature fluctuation ≤ ±0.3 °C, uniformity ≤ ±2.0 °C, fully compliant with GR-468 linearity and consistency requirements • Mass production adaptability: Compact chamber structure with multi-layer sample racks, supporting batch screening of hundreds of optical engines per cycle, matching mass production ESS screening rhythm 5.2 System & Rack-level Solution: Walk-in Rapid Temperature Change Chamber For full CPO switch system and server cabinet verification, Lab Companion provides large-scale walk-in temperature cycling chambers: • Volume range: 1,000L–10,000L • Load capacity: 1,000 kg mechanical load, supporting 50 kW DUT self-heating test • Working conditions: -20 °C ~ +55 °C, temperature rate ≥ 5 °C/min • Application: Full-system loaded temperature cycling test for complete CPO switching platforms 5.3 MES docking & full data traceability All Lab Companion test chambers support real-time recording of temperature curves, rate changes, and dwell data. Equipped with standard Ethernet and RS485 interfaces, and optional OPC UA / Modbus TCP protocols, the equipment can seamlessly connect with factory MES systems to build full-lot, full-process quality traceability, meeting international certification audit requirements. 6. Reliability Determines the Long-term Commercial Value of CPO The global CPO market is transitioning from technical verification to large-scale manufacturing. In the next 3–5 years, the core competition of CPO products will focus on mass-production reliability rather than basic technical implementation. From micro-level optical engine stress screening to full-system cabinet-level thermal verification, Lab Companion (China High-end Manufacture) provides standardized, compliant, and efficient temperature cycling test solutions for global CPO and optical communication clients. With reliable Chinese manufacturing quality and professional overseas online after-sales system, Lab Companion supports global customers throughout the entire R&D verification and mass production screening process. As CPO market penetration grows from 0.5% (2026) to 35% (2030), standardized and high-precision environmental reliability test equipment will remain the core guarantee for product long-term stable operation.
    EN SAVOIR PLUS
  • Lab Companion|From Consumer SSDs to High-Speed Optical Modules: Expanding Boundaries of Environmental Reliability Testing Lab Companion|From Consumer SSDs to High-Speed Optical Modules: Expanding Boundaries of Environmental Reliability Testing
    Sep 24, 2026
    1. Evolving Testing Scenarios: Wider Application Coverage Across High-Tech Industries Environmental reliability testing was once dominated by automotive and industrial applications. Today, the testing landscape has expanded rapidly to serve fast-growing high-tech sectors, including consumer storage, high-speed optical communication, semiconductors, and AI computing hardware. Reliability validation has become a mandatory prerequisite for mass production. Consumer electronics no longer require only basic functionality—they demand stable performance across diverse and harsh climatic conditions. The booming deployment of high-speed optical modules for AI data centers further raises the bar for temperature cycling and environmental durability testing. In this competitive market, product consistency, scenario adaptability, and professional testing capabilities have become core benchmarks for global supplier selection. 2. Consumer SSDs: Strict Temperature Cycling Reliability Requirements Consumer SSDs operate under far more complex thermal conditions than standard room-temperature environments. Heavy-load laptop operation, industrial storage deployment, and cross-region mobile usage continuously expose SSD controllers, flash particles, and power circuits to repeated thermal cycling stress. SSD mass testing features two key challenges:large sample volume and cost-effective validation. Lab Companion rapid temperature change test chambers, equipped with multi-layer sample racks, enable high-volume thermal stress screening with precisely controlled temperature rates and cycle times. The solution effectively eliminates early failures while optimizing testing costs. Beyond basic thermal cycling, SSD testing requires full data integrity monitoring throughout the entire test process. Lab Companion systems support seamless integration with third-party storage monitoring tools, synchronizing temperature curve recording and device status logging. This enables engineers to accurately identify failure root causes—whether from environmental thermal stress or firmware logic issues—and ensures complete, traceable test data for certification and R&D iteration. 3. Optical Modules & Passive Optical Components: Non-Negotiable Thermal Cycling Validation Temperature cycle reliability testing is an essential and standardized procedure for optical communication devices. Laser wavelength accuracy and output optical power are highly sensitive to temperature fluctuations, while fiber coupling structures are prone to thermal deformation. Both active optical modules and passive components such as wavelength division multiplexers and optical isolators must undergo full environmental validation in accordance with international standards including GR-468. High-value optical communication devices prioritize testing accuracy and depth over speed. Lab Companion environmental test chambers reserve abundant external interface resources, supporting multi-channel synchronous temperature acquisition and real-time monitoring of optical power, extinction ratio, and other critical optical parameters. This synchronized testing mechanism builds a complete data chain to support product certification, performance optimization, and mass production quality control. 4. Core Equipment Selection Criteria for Diverse High-Tech Testing As testing scenarios diversify from traditional automotive applications to consumer storage and optical communication, global clients have formed three clear selection principles: Scenario-oriented customization. SSD production requires high-throughput batch screening capacity; optical device testing demands multi-point temperature acquisition and external instrument compatibility; large-scale product validation relies on spacious chamber volume and high-load thermal stability. Professional testing requires scenario-matched equipment rather than generalized models. Certified and verified manufacturing strength. Global buyers prioritize actual loaded performance data, standardized management systems, and stable long-term quality. Lab Companion holds ISO9001, ISO14001, ISO45001, ISO27001 and CE certifications, with full international trademark protection under the Madrid System, delivering globally recognized quality and compliance. Complete data traceability. Advanced electronics and optical industries require standardized test archives and fully traceable experimental data. All Lab Companion equipment supports automatic data recording, intelligent report export, and full-process data retention, meeting strict international audit and certification requirements. In addition, turnkey laboratory procurement has become mainstream. Lab Companion supports integrated delivery of rapid temperature change chambers, temperature & humidity chambers, thermal shock chambers, and walk-in environmental rooms, with unified temperature control logic and standardized data formats for unified laboratory management. 5. Lab Companion: Premium Chinese Manufacturing, Global Standard Test Solutions Rooted in China, serving the world. As a leading high-tech and specialized enterprise based in Dongguan, China, Lab Companion boasts 21 years of professional R&D and manufacturing experience in environmental reliability testing equipment. Benefiting from China’s mature high-end equipment manufacturing industrial chain, we deliver cost-effective, high-precision, and durable testing solutions for global clients across semiconductor, optical communication, consumer electronics, automotive, and research sectors. Our flagship TC series rapid temperature change chambers cover a wide temperature range of -70℃ to +150℃ with customizable specifications. The actual loaded temperature change rate reaches 5–25℃/min, up to 30℃/min with liquid nitrogen assistance. Multiple volume options from 80L to 1000L fully adapt to SSD batch screening and high-precision optical component testing. Extended 24-channel temperature acquisition and external instrument docking capability support professional-grade optical communication reliability verification. Optional alternating humidity modules provide 20%–98% RH adjustable humidity range, fully complying with GR-468 and other international industry standards. Standard anti-condensation design, programmable cycle editing, and full data traceability ensure stable and repeatable test results. Supported by three major manufacturing bases in China (Dongguan, Kunshan, Chongqing) with an annual production capacity of over 2,000 units, Lab Companion delivers stable batch delivery capability for global orders. For overseas clients, we provide professional online technical guidance, remote debugging, and lifelong online after-sales support, ensuring efficient project implementation and stable equipment operation without local on-site service. 6. Professional Reliability Testing Empowers Global Tech Innovation As high-tech industries continue to iterate globally, diversified application scenarios raise higher requirements for environmental reliability verification. Professional, standardized, and scenario-tailored testing is the solid foundation for product stability and global market compliance. Adhering to the rigorous craftsmanship of Chinese high-end equipment manufacturing, Lab Companion focuses on technological innovation and scenario customization. We provide global clients with one-stop, high-reliability environmental testing solutions, supporting R&D iteration, international certification, and high-quality mass production of global technological products.
    EN SAVOIR PLUS
  • From Scale Expansion to Quality Upgrade: 21 Years of Environmental Test Equipment Innovation by Lab Companion in Dongguan, China
    Sep 18, 2026
    1. A Defining Turning Point for China’s Environmental Test Equipment Industry In 2026, China’s environmental test equipment industry enters a pivotal transformation phase. After years of scale-driven growth, the sector is now shifting toward high-quality performance, technological sophistication, and high-end localization. Driven by booming demand across optical modules, semiconductors, and AI computing infrastructure, the industry’s competition logic has fundamentally changed—from simple capacity expansion to comprehensive strength in precision, stability, and system reliability. The domestic Chinese market for environmental test chambers has surpassed ¥18.5 billion in 2026. Localized manufacturing penetration has reached 58.7%, while Chinese brands capture 76.8% of the overall market share. This data proves that Chinese substitution is no longer limited to low-end equipment; it is rapidly penetrating high-precision and mission-critical application fields. As a leading Chinese manufacturer rooted in Dongguan’s advanced manufacturing cluster, Lab Companion answers one core industry question: how Chinese-engineered environmental test equipment is replacing imported solutions through decades of accumulated R&D and manufacturing expertise. 2. Strong Downstream Demand Reshapes Global Testing Standards 2.1 Optical Modules: Test Equipment Becomes a Production-Critical Necessity The global high-speed optical module industry is undergoing massive capacity expansion in 2026. Annual shipments are expected to reach 45 million units for 800G modules and 33 million units for 1.6T modules, with 1.6T demand projected to double in 2027. As optical communication systems advance, testing accuracy requirements have become extremely stringent. DFB lasers inside high-speed optical modules feature a wavelength drift coefficient of only 0.08–0.1 nm/°C. In 100 GHz DWDM systems, minor temperature deviations can cause severe crosstalk and increased bit error rates. Compliant with the GR-468-CORE global standard, production validation requires thermal cycling ranging from -40°C to +85°C with a linear temperature change rate of no less than 10°C/min. Under such strict specifications, reliable environmental test chambers have evolved from optional auxiliary devices into indispensable core production equipment for global optical module manufacturers. 2.2 Semiconductor & AI Computing Growth Drives High-End Testing Upgrades China’s semiconductor industry continues large-scale capacity upgrades. In 2026, domestic wafer fabrication and packaging firms announced expansion projects totaling over ¥45 billion in investment. Advanced semiconductor processes demand stricter temperature stability and cycling accuracy, making environmental test chambers essential for chip design verification, wafer manufacturing, and packaging reliability validation. Meanwhile, global AI computing infrastructure is experiencing explosive growth. China’s AI computing demand surged 417% year-on-year in Q1 2026. Modern AI chips commonly exceed 200W power consumption, making hardware highly sensitive to repeated thermal shocks. Temperature fluctuations can cause packaging delamination, solder joint cracking, and long-term performance degradation. This industry trend creates strong global demand for high-load, fast temperature change test solutions capable of simulating real-world operating stress. 3. Industry Competition Shifts from Scale Growth to Technical Quality 3.1 New Competition Focus: Real-World Stability Over Paper Parameters The industry’s competitive benchmark has undergone a major upgrade since 2022. Four years ago, most manufacturers competed on empty-chamber specifications, prioritizing maximum temperature range and top heating/cooling rates. At that time, Chinese brands held only 35% of the mid-to-high-end market. By 2026, customer evaluation standards have matured significantly. Global buyers now prioritize full-load stability, temperature uniformity, long-duration operational reliability, and energy efficiency rather than theoretical parameters. The mid-to-high-end market penetration of Chinese equipment has risen to 58%, marking a decisive shift from low-cost scale expansion to high-value technological competition. 3.2 Localization Enters the High-End Breakthrough Stage China’s independent equipment manufacturing capability continues to improve. The overall localization rate of environmental test equipment increased from 49.6% in 2024 to 52.7% in 2026. Chinese-made equipment has achieved 35.4% penetration in new energy vehicle testing and 28.6% in aerospace reliability verification. Chinese manufacturers deliver clear global advantages: cost-performance, flexible customization, and efficient technical support. While imported equipment still retains marginal advantages in ultra-high precision and extreme fast thermal cycling, Chinese-manufactured solutions are rapidly closing the technological gap and becoming the preferred alternative for global mass production and reliability validation scenarios. 4. Lab Companion: 21 Years of Premium Manufacturing Rooted in China’s Dongguan Industrial Cluster 4.1 China-Based Production Layout: Three Advanced Manufacturing Bases Founded in 2005, Lab Companion is a professional environmental reliability test equipment manufacturer deeply rooted in Dongguan, Guangdong Province—one of China’s most advanced and comprehensive high-tech manufacturing hubs. Benefiting from Dongguan’s complete industrial supply chain, precise component processing capabilities, and mature electronic manufacturing ecosystem, Lab Companion has grown into a globally competitive Chinese brand over 21 years of focused development. The company operates three major R&D and manufacturing bases in Dongguan, Kunshan, and Chongqing, covering a total factory area of 27,286 m² with an annual production capacity of approximately 2,000 units. The product portfolio includes more than 30 categories: temperature & humidity chambers, rapid thermal cycling chambers, thermal shock chambers, HAST accelerated life testers, and large walk-in environmental laboratories. Lab Companion provides full-level reliability testing solutions from component-level verification to complete machine and cabinet-level validation. 4.2 Independent R&D and Global Standard Certification System As one of China’s earliest environmental test equipment manufacturers certified with CE compliance, Lab Companion holds internationally recognized trademarks registered under the Madrid System, covering the EU, UK, Canada, Southeast Asia, and other global regions. The company maintains strict international management standards, including ISO 9001 Quality Management, ISO 14001 Environmental Management, ISO 45001 Occupational Health & Safety, and ISO 27001 Information Security certifications. With independent intellectual property rights in core temperature control algorithms and refrigeration optimization technologies, Lab Companion was officially recognized as a China “Specialized, Refined, Advanced, and Innovative Enterprise” in 2026, achieving full self-control of core technologies. 4.3 High-Precision Products Tailored for Global High-End Scenarios To meet stringent testing requirements for optical modules and semiconductors, Lab Companion’s rapid temperature change series covers a temperature range of -70°C to +150°C, with five adjustable rate levels from 5°C/min to 25°C/min. All cooling and heating rates are verified under full-load operating conditions, ensuring consistent and reliable real-world performance for global production lines. For high-power AI server and GPU testing scenarios, Lab Companion has developed dedicated high-load thermal cycling equipment supporting up to 50kW continuous heat load, effectively solving thermal fatigue, delamination, and solder failure challenges for high-power computing hardware. The self-developed C100 PID fuzzy logic temperature and humidity control system delivers 28%–38% lower energy consumption than the industry average, enabling high precision, high stability, and energy efficiency for global clients. 5. Global Direct Factory Model & Overseas Remote Technical Support Environmental test equipment features strong non-standard customization characteristics. Traditional multi-layer distribution channels often cause delayed communication, inconsistent technical understanding, and increased procurement costs. Lab Companion adopts a direct factory sales model worldwide, enabling global customers to communicate directly with professional R&D and engineering teams without intermediate dealers. Supported by three intelligent manufacturing bases in China, Lab Companion flexibly allocates production resources to ensure stable lead times even during peak global order seasons. Customers obtain genuine factory-direct pricing, customized technical solutions, and consistent production quality. For global overseas clients, Lab Companion provides professional online remote guidance and full-cycle technical support. Unlike regional domestic on-site services, the global support system delivers fast online troubleshooting, equipment calibration guidance, operational training, and remote system optimization, ensuring stable and continuous equipment operation for overseas production and laboratory facilities. 6. Conclusion: Chinese Manufacturing Moves from Scale Advantage to Technical Leadership China’s environmental test equipment industry is undergoing a historic transformation from quantitative expansion to qualitative upgrading. Fueled by global growth in optical communication, semiconductors, and AI computing, Chinese manufacturers are stepping onto the global stage, competing through core precision, stability, and systematic service capabilities rather than low-cost advantages. With 21 years of manufacturing heritage rooted in China’s Dongguan industrial cluster, three national production bases, full-coverage high-end product lines, and efficient global direct service mechanisms, Lab Companion represents a new generation of Chinese high-end equipment brands. As the global industry shifts from scale competition to quality competition, Lab Companion continues to deliver reliable, cost-effective, and technologically advanced testing solutions, establishing a trusted benchmark for Chinese-manufactured environmental test equipment worldwide.
    EN SAVOIR PLUS
  • Lab Companion High-Low Temperature Test Chamber: Endurance Testing for Long-Term Continuous Operation of High-Power Servers Lab Companion High-Low Temperature Test Chamber: Endurance Testing for Long-Term Continuous Operation of High-Power Servers
    Sep 15, 2026
    1. Demands for Long-Duration Continuous Server Operation Testing 1.1 24/7 Server Operation Demands High Endurance from Test Equipment High-power servers deployed in data centers require stable 24/7 continuous operation. Long-term exposure to ambient temperature fluctuations and gradual heat dissipation degradation leads to cumulative thermal stress, causing component aging, performance drift, and unexpected hardware failures. For AI training servers, continuous full-load tasks can last for days or even weeks, resulting in severe heat accumulation and accelerated component fatigue. Short-term functional verification cannot fully reflect real-world server reliability. Long-duration high-temperature continuous testing is essential to expose latent defects triggered by prolonged thermal stress. In such reliability validation scenarios, the long-term operational stability of the test chamber directly determines the accuracy and credibility of test data. 1.2 Industry Standards for Long-Term High-Temperature Aging Testing High-temperature aging testing is a mandatory reliability procedure for server systems. Servers are placed in a constant high-temperature environment of +40℃ to +55℃ and run full-load stress tests on CPUs, memory, and storage devices. Standard test durations range from 48 to 72 hours, while reliability growth tests can extend to hundreds of hours. GB/T 2423.2-2018 specifies a test temperature range of 40℃ to 85℃ for server motherboard high-temperature testing, with adjustable test durations from 24 hours to hundreds of hours and real-time performance monitoring requirements. GB/T 9813.3-2017 mandates a minimum server MTBF (Mean Time Between Failures) of 10,000 hours, requiring 168 hours of fault-free full-load continuous operation. These industry standards strictly require environmental test equipment to maintain precise and stable temperature output during ultra-long continuous operation. 2. Core Technical Advantages of Lab Companion High-Low Temperature Test Chambers for Long-Duration Operation 2.1 Superior Long-Term Temperature Field Stability Lab Companion high-low temperature test chambers feature a wide temperature range of -70℃ to +150℃, with a temperature fluctuation of 0.5℃ and a temperature deviation of ±2℃. While precise temperature control is easy to achieve in short-term tests, maintaining zero drift during hundreds of hours of continuous operation requires systematic optimized design. Equipped with the C100 PID + fuzzy logic control system, the chamber supports automatic self-checking, linear temperature and humidity calibration, and intelligent automatic shutdown. The balanced temperature and humidity control strategy precisely matches heating and cooling output, effectively reducing frequent compressor startup and shutdown and ensuring long-term operational stability. The standard heating rate is approximately 3℃/min (20℃ to +150℃), and the cooling rate is 1.2℃/min (20℃ to -70℃). The chamber can operate stably for hundreds of hours continuously with consistent temperature distribution across the entire test cavity, ensuring uniform thermal stress for all test samples. 2.2 Long-Life Core Component Design for Continuous Workloads To adapt to ultra-long uninterrupted testing scenarios, Lab Companion adopts high-reliability industrial-grade configurations. Key models are equipped with dual-compressor redundant design (one working, one standby), which automatically switches units in case of single compressor failure to avoid test interruption. Built-in soft start and soft stop protection avoids instantaneous current impact; a 3-minute compressor delay protection mechanism effectively extends component service life. The inner chamber adopts SUS304 stainless steel, and all sealing parts use high and low temperature resistant silicone rubber materials, providing excellent aging resistance for long-cycle testing. 2.3 Strict Factory Endurance Verification All Lab Companion test chambers undergo full-load aging tests before delivery to simulate the harshest on-site working conditions. New product models complete more than 1,000 hours of reliability endurance testing, and all finished products pass 72-hour continuous operation, temperature uniformity, and safety protection verification. Internal test data shows that after simulated 3-year uninterrupted operation tests, the temperature rate attenuation is ≤5% and the temperature accuracy attenuation is ≤0.1℃, far better than the industry average of 15%. The redundant system design increases the MTBF by 2.5 times compared with traditional single-unit equipment under 3,000-hour continuous operation conditions. 3. Practical Testing Solutions for High-Power Server Long-Duration Operation 3.1 Standard High-Temperature Continuous Test Procedures Place the server unit inside the test chamber and raise the temperature to the target value (55℃ or 70℃ typical) at a rate no more than 1℃/min. Start formal timing after the internal temperature field stabilizes. Keep the server running full-load stress programs throughout the test, and continuously monitor CPU/GPU temperature, power consumption, fan speed, and system logs. Lab Companion chambers support scheduled startup and automatic timed shutdown, enabling unattended long-cycle testing and avoiding energy waste and idle operation risks. 3.2 Key Control Factors for Long-Cycle Testing Consistent Temperature Uniformity for Multi-Server Parallel TestingLarge-capacity models (600L/1000L/1500L) support simultaneous testing of multiple server units. With a temperature uniformity within ±2.0℃, the chamber ensures identical thermal stress conditions for all samples during long-duration batch testing. Traceable Test Data RecordsThe system automatically records full-process temperature curves and alarm logs, supporting complete data review and abnormal cause analysis after long-cycle testing, ensuring test authenticity and repeatability. Multi-Layer Hardware Protection Prevents Test InterruptionIndependent over-temperature protectors, mechanical pressure switches, and thermal relays provide hardware-level safety isolation, responding within milliseconds to avoid equipment failure and test data loss during hundred-hour continuous tests. 4. Conclusion Lab Companion high-low temperature test chambers deliver reliable, stable, and repeatable environmental simulation for high-power server high-temperature aging and long-duration reliability verification. With a wide temperature range of -70℃ to +150℃, precise temperature control accuracy, and industry-leading long-term operational stability, the equipment fully meets standard 48–72 hour aging tests and ultra-long reliability growth tests of hundreds or thousands of hours. As a professional environmental test equipment brand, Lab Companion provides global customers with standardized equipment and customized reliability test solutions for server, electronics, and semiconductor industries.
    EN SAVOIR PLUS
  • Lab Companion Rapid Temperature Change Test Chamber: Long-Term Stability Ensures Server Reliability Data Credibility
    Sep 14, 2026
    1. The Overlooked Factor: Long-Term Stability of Test Equipment 1.1 Server Reliability Testing Demands Stable Endurance from Test Chambers High-power servers, especially AI training servers, require continuous 7×24 full-load operation in real scenarios. Large-model training tasks often run for days or weeks continuously. Long-duration thermal accumulation accelerates component aging and gradually introduces performance drift and hidden hardware failures. Therefore, server reliability validation cannot rely solely on short-term functional tests. It requires long-duration high-temperature aging tests to expose potential defects caused by sustained thermal stress. Global mainstream standards define clear testing requirements: • GB/T 2423.2-2018: Server motherboard high-temperature test range from 40℃ to 85℃, with test durations ranging from 24 hours to hundreds of hours. • GB/T 9813.3-2017: Server MTBF must exceed 10,000 hours, requiring 168 hours of continuous full-load aging without failure. These strict standards require environmental test equipment to maintain precise and stable conditions for hundreds of hours. In most procurement evaluations, buyers focus heavily on temperature range, ramp rate, and chamber volume, while easily ignoring long-term precision retention — the most critical factor that determines whether server test data is trustworthy. 1.2 How Equipment Drift Misleads Server Reliability Judgments After long-term cyclic operation, test chambers gradually generate parameter drift due to sensor aging, controller offset, and refrigeration system performance degradation. Subtle deviations in temperature accuracy, uniformity, and ramp rate will not trigger obvious equipment alarms, but they directly invalidate long-duration server test results. In high-power server full-load testing, even a 0.5℃ undetected temperature deviation can mask thermal design weaknesses. Poorly optimized server hardware may pass qualification tests mistakenly, bringing severe reliability risks to mass production and data center long-term operation. 2. Root Causes of Precision Degradation & Lab Companion Hardware Solutions 2.1 Three Core Causes of Long-Term Precision Loss Precision degradation is a cumulative aging effect, mainly derived from three systems: 1) Sensor drift Platinum sensors working repeatedly between -70℃ and +150℃ experience gradual resistance drift. Even minor deviations of 0.1℃–0.2℃ are enough to change the pass/fail judgment of high-precision server and semiconductor reliability tests. 2) Control algorithm offset Traditional fixed PID parameters are calibrated under no-load conditions. After long-term full-load server testing, original control parameters no longer match actual thermal loads, causing temperature overshoot, fluctuation, and unstable ramp speed. 3) Refrigeration and airflow decay Compressor efficiency attenuation, condenser dust accumulation, and fan wear gradually destroy internal temperature uniformity, resulting in inconsistent thermal stress for multi-server parallel testing. 2.2 Lab Companion Redundant Hardware Design for Long-Term Stability Lab Companion TC series rapid temperature change chambers adopt systematic anti-aging and redundant design to avoid long-term precision attenuation, fully adapting to server ultra-long-duration full-load tests. Dual-compressor redundant refrigeration system High-speed and low-temperature models are equipped with dual-compressor backup design (one working, one standby). The system automatically switches in case of single-unit failure, ensuring zero test interruption during hundreds of hours of continuous server aging tests. Dual compressors dynamically adjust load operation to avoid long-term full-load fatigue loss. Comprehensive component protection mechanism Soft start and soft stop systems eliminate instantaneous current impact. A minimum 3-minute compressor delay protection effectively extends service life. Built-in hot gas bypass valves stabilize pressure under variable loads and reduce frequent compressor start-stop fluctuations. Durable chamber and sealing structure Adopting SUS304 stainless steel inner chamber and high and low temperature resistant silicone seals, the equipment maintains stable physical performance after thousands of temperature cycles. The stable technical specifications cover -70℃ to +150℃, with temperature fluctuation ≤0.5℃ and temperature deviation within ±2℃. 3. Full-Lifecycle Stability Assurance: Factory Validation + On-Site Operation 3.1 Strict Factory Aging Validation Every Lab Companion chamber completes full-load aging before delivery to simulate the harshest customer working conditions. • New products pass 1,000+ hours reliability endurance tests • All finished products pass 72-hour continuous stable operation inspection Official test data proves that after simulated 3-year non-stop operation, with anti-fatigue structure and dynamic compensation algorithm: • Temperature ramp rate attenuation ≤5% (industry average: 15%) • Temperature accuracy attenuation ≤0.1℃ • Redundant system MTBF increases 2.5 times compared with traditional single-compressor systems 3.2 Industrial Long-Duration Operation Verification A leading automotive semiconductor packaging enterprise in East China deployed two Lab Companion HZ-ESS-800L rapid temperature change chambers (15℃/min ramp rate) for 7×24 batch cyclic reliability testing. With only 4-hour maintenance every two weeks, the units have achieved more than 5,000 hours of non-stop stable operation by Q1 2025. No unplanned shutdown occurred. Customer on-site logs show compressor current, exhaust pressure, and superheat parameters remain stable without long-term drift, fully proving long-term operational consistency under continuous heavy-load conditions. 3.3 Standardized Maintenance System to Sustain Long-Term Accuracy Lab Companion provides a standardized precision maintenance mechanism for long-term server testing scenarios. Users can perform quarterly sensor calibration with CNAS-certified tools or acquire official on-site calibration services. With standardized maintenance logs and annual professional inspection, the chamber consistently maintains high precision: temperature accuracy ±0.1℃~±0.3℃ and temperature uniformity ≤±0.5℃, fully meeting international reliability test standards. 4. Key Operation Guidelines for High-Power Server Testing To ensure credible and repeatable server long-duration test results, three key principles should be followed: 1) Quarterly sensor calibration Long-hour testing accumulates subtle sensor drift. Regular calibration eliminates system errors and ensures authentic thermal stress conditions. 2) Continuous operation log analysis Monitoring compressor status, pressure data, and temperature curve trends enables early detection of performance degradation and avoids unexpected test termination. 3) Full-load temperature uniformity verification High-power servers generate strong self-heating during full-load operation. Ensure chamber temperature uniformity remains stable under heavy load to guarantee consistent test conditions for single or multiple parallel server units. 5. Conclusion Server reliability testing aims to verify long-term operational stability under extreme and continuous thermal stress. The credibility of test results fundamentally depends on the long-term precision stability of the test chamber. Lab Companion rapid temperature change test chambers eliminate long-term drift, unexpected shutdowns, and data inconsistency through redundant hardware design, strict factory aging validation, and standardized lifecycle maintenance systems. The equipment fully supports conventional 48–72 hour server aging and hundreds-to-thousands of hours high-level reliability growth testing. As a professional environmental test equipment brand with 21 years of R&D and manufacturing experience, Lab Companion provides global customers with stable, repeatable, and traceable environmental test solutions, as well as full-cycle technical support from solution customization to after-sales service.
    EN SAVOIR PLUS
  • Lab Companion Temperature Cycling Chamber: AEC-Q100 Qualification Test Practice for Automotive eMMC / UFS / SSD
    Sep 09, 2026
    1. Practical Requirements of AEC-Q100 Qualification for Automotive Storage 1.1 Market Entry Barriers for Automotive-Grade Storage Driven by vehicle intelligence and connectivity, automotive storage devices are seeing rising adoption. Infotainment systems, instrument clusters, T-BOX units, ADAS domain controllers and autonomous driving domain controllers all rely on eMMC, UFS or automotive SSD for data storage. Unlike consumer storage, automotive storage directly impacts driving safety and user experience, requiring far higher reliability. Tier 1 suppliers and OEMs universally mandate AEC-Q100 reliability qualification for storage components during part selection. Products without this qualification cannot be admitted into automotive supply chains. AEC-Q100 is an IC stress test specification defined by the Automotive Electronics Council. It specifies a full suite of reliability tests for automotive ICs before mass release, including temperature cycling, high-temperature operating life, high temperature humidity bias, ESD and latch-up. Temperature cycling is one of the core tests. It verifies package integrity and solder joint fatigue life under repeated thermal swings. For automotive storage, temperature cycling results determine whether a product can pass AEC-Q100 and be listed in OEM approved vendor lists. 1.2 Position of AEC-Q100 in Storage Component Qualification AEC-Q100 classifies devices into four temperature grades based on operating temperature ranges for different vehicle applications: • Grade 3: 0℃ to +85℃ • Grade 2: -40℃ to +105℃ • Grade 1: -40℃ to +125℃ • Grade 0: -40℃ to +150℃ Grade 3 applies to less demanding in-cabin infotainment systems. Grade 2 covers body control, infotainment and T-BOX, which represent most automotive electronic modules. Grade 1 targets harsh environments near engine bays and ADAS domain controllers. Grade 0 serves the most demanding engine and transmission control units. For automotive storage, Grade 2 and Grade 1 are the mainstream qualification levels. Storage for infotainment and body control typically follows Grade 2. ADAS and autonomous driving storage, mounted close to engine compartments or requiring higher reliability margin, usually requires Grade 1. Temperature cycling is a mandatory AEC-Q100 test. Test conditions vary by grade: Grade 2 uses -40℃ to +105℃; Grade 1 uses -40℃ to +125℃. Both require a minimum of 500 cycles. 2. Comparison of Temperature Cycling Conditions: Grade 1 vs Grade 2 2.1 Grade 2: -40℃ ~ +105℃ Condition Breakdown Grade 2 temperature cycling spans -40℃ to +105℃ with a 145℃ delta. This profile simulates extreme real-world cabin conditions: vehicles parked outdoors in cold northern winters may drop near -40℃; after summer sun exposure, electronics behind dashboards can exceed 100℃. Each cycle consists of four phases: ramp from -40℃ to +105℃ (typically 10℃/min to 15℃/min), dwell at +105℃ for ≥10 minutes to stabilize internal sample temperature, ramp down from +105℃ to -40℃, then dwell at -40℃ for ≥10 minutes. One full cycle takes roughly 40–60 minutes. 500 cycles require continuous chamber operation for 330–500 hours (14–21 days). Samples remain powered during cycling, with real-time monitoring of read/write performance and key parameters. 2.2 Grade 1: -40℃ ~ +125℃ Condition Breakdown Grade 1 uses -40℃ to +125℃, creating a 165℃ temperature delta. Compared with Grade 2, the upper temperature limit rises by 20℃ and the thermal delta increases by 20℃. This profile targets storage mounted near engine bays and ADAS controllers, where component temperatures can exceed 105℃ and reach above 120℃ under heavy vehicle load. Raising the maximum temperature to 125℃ substantially increases stress on storage devices: 1. Larger thermal expansion mismatch across different materials creates stronger thermo-mechanical stress on solder joints and package interfaces, accelerating defect exposure. 2. 125℃ approaches the glass transition and creep range of molding compounds and solders, degrading mechanical properties and raising risks of solder fatigue and package delamination. 3. High temperatures accelerate NAND Flash data retention degradation, imposing stricter reliability requirements on storage media. The cycle sequence matches Grade 1 and Grade 2. However, the wider temperature delta extends ramp times. One Grade 1 cycle lasts 50–70 minutes. Completing 500 cycles requires continuous operation for 420–580 hours (18–24 days). 2.3 Test Differences and Selection Logic The core distinction between Grade 1 and Grade 2 lies in maximum temperature and thermal delta, which affects three areas: thermal stress magnitude, total test duration and chamber requirements. Grade 1 generates higher thermal stress and accelerates latent failure modes. Its total test time is 20–30% longer. The 125℃ plateau demands superior heating performance and temperature stability without overshoot. When defining qualification strategy, select the grade based on end application. Grade 2 is sufficient for infotainment, body control and T-BOX. Grade 1 is recommended for ADAS, autonomous driving controllers, engine-bay adjacent hardware, global markets or applications requiring extra reliability margin. A Grade 1 qualified component is backward compatible with Grade 2 use cases, while Grade 2 parts cannot be deployed in Grade 1 environments. Many manufacturers choose Grade 1 qualification upfront to broaden market coverage. 3. Full Workflow of Temperature Cycling Test 3.1 Pre-test: Sample Preparation and Initial Characterization AEC-Q100 temperature cycling includes three phases: pre-test preparation, test execution and post-test evaluation. Pre-test work ensures consistent sample condition and complete baseline data. A minimum of 77 units are randomly sampled from one batch (exact quantity depends on test plan and acceptance criteria). All samples undergo visual inspection to rule out physical damage, package defects or marking issues. Initial electrical characterization is then performed and recorded: functional tests (read/write, erase, bad block management), performance tests (sequential read/write speed, random IOPS), and health checks including SMART attributes, bad block count, wear leveling and initial error rates. Baseline data serves as reference for post-test comparison. Any meaningful parameter shift must be documented and analyzed. Only samples passing initial inspection are loaded into the chamber. Sample loading rules: distribute samples evenly across shelves to avoid localized thermal accumulation. Mount each unit on sockets or burn-in boards connected to external test hosts for live power monitoring. Maintain sufficient air gaps between samples to prevent airflow blockage and temperature non-uniformity. 3.2 Test Execution: Program Setup, Live Monitoring and Cycle Counting During execution, the chamber controller runs a programmed thermal profile: start temperature, ramp rate, high dwell setpoint and duration, low dwell setpoint and duration, plus target cycle count. Grade 2 is programmed for -40℃ / +105℃; Grade 1 for -40℃ / +125℃. Ramp rates are set between 10℃/min and 15℃/min, with minimum 10-minute dwells at extremes and 500 total cycles. Once started, the chamber runs automatically and continuously logs thermal profiles. External test hosts maintain power to DUTs and collect data every 5–10 minutes. Monitored items include power status, read/write integrity, disk dropouts, communication interruptions and abnormal error growth. Critical events such as DUT dropout are timestamped with cycle number. Cycle counting adopts dual control: automatic chamber logging plus daily manual cross-check against temperature curves to confirm validity. If tests stop due to power loss, chamber fault or temperature alarm, engineers review logs and thermal history to decide whether partial cycles count toward the total. AEC-Q100 defines clear rules for interrupted tests; all decisions must follow the standard. 3.3 Post-test: Final Characterization, Failure Analysis and Report Generation After finishing 500 cycles, samples are removed and stabilized for ≥2 hours under standard ambient conditions (15℃–35℃, 25–75% RH) before final testing. Final tests repeat the full initial inspection suite: visual check, functional, performance and health assessment. Acceptance criteria: no visible cracking, deformation or package damage; all read/write functions remain operational without dropouts or communication failures; performance degradation stays within product specification limits; bad block and error count increases remain within acceptable thresholds. Any failed unit triggers failure investigation. AEC-Q100 uses LTPD sampling to determine batch pass/fail based on failure tally. Failed samples go through failure analysis: SAM scanning for package delamination, X-ray inspection for solder cracking, cross-sectioning to observe crack morphology, and electrical fault isolation. FA findings feed design and process improvements. The final test report contains standard reference, test profile, chamber ID/calibration status, sample batch/serial numbers, baseline data, continuous temperature logs, cycle records, real-time monitoring logs, post-test results and failure analysis conclusions. Reports require sign-off by test and review engineers as supporting documentation for AEC-Q100 certification. 4. AEC-Q100 Compliance Capabilities of Lab Companion Temperature Cycling Chambers 4.1 Temperature Range and Accuracy Compliance Lab Companion temperature cycling chambers cover -70℃ ~ +150℃, fully satisfying AEC-Q100 Grade 2 (-40℃ to +105℃) and Grade 1 (-40℃ to +125℃) requirements with ample safety margin. The system maintains stable long-run operation at 125℃ without thermal drift. Performance specifications: temperature fluctuation ≤ ±0.5℃, temperature uniformity ≤2.0℃, temperature deviation ±2.0℃, exceeding GB/T 5170 requirements. AEC-Q100 requires consistent thermal stress across all DUTs. Lab Companion’s ≤2.0℃ uniformity ensures all automotive storage samples experience equivalent thermal loading over 500 cycles, delivering statistically valid test results. Linear ramp rates are configurable from 5℃/min to 25℃/min to precisely replicate AEC-Q100 thermal profiles. 4.2 Long-duration Stability and Data Traceability AEC-Q100 temperature cycling demands uninterrupted operation for 14–24 days. Lab Companion chambers use premium brand compressors and refrigeration components with multi-layer protection: over-temperature, compressor overload and phase-loss protection. Every unit undergoes a minimum 48-hour continuous run-in test before shipment to validate refrigeration and control reliability. Traceability is mandatory for AEC-Q100 audits. The touch controller automatically records temperature curves, cycle counters, alarms and runtime logs. Data can be exported via USB as CSV or PDF files for report archiving. Complete thermal logs serve as objective evidence during certification audits and meet traceability requirements. 4.3 Calibration at Dongguan Factory & Global Service Support Each chamber is assembled and calibrated at the Dongguan manufacturing site. Factory validation includes ramp rate verification, 9-point temperature mapping, extreme setpoint stability testing and continuous runtime validation. For automotive storage customers, pre-run validation for Grade 1 or Grade 2 profiles can be performed to confirm performance under your target test conditions. Delivery includes calibration certificates and validation reports, ready for lab system audits and AEC-Q100 on-site reviews. Our global service network delivers installation, commissioning, periodic calibration and on-site repair. Automotive qualification schedules are tight; rapid service response minimizes downtime caused by equipment faults. Annual maintenance is recommended, including refrigeration inspection, electrical tightening, thermal field recalibration and consumable replacement to sustain accuracy for years of AEC-Q100 testing. 5. Common Issues in AEC-Q100 Qualification and Mitigation 5.1 Test Interruption and Cycle Recounting Power outages, equipment faults or temperature alarms may halt cycling. AEC-Q100 interruption rules: if the stop occurs during temperature dwell, lasts ≤30 minutes and sample temperature remains close to setpoint, completed cycles remain valid. If interruption happens during ramp-up/ramp-down, or temperature deviates significantly, the incomplete cycle is discarded and valid counts must be re-evaluated against thermal logs. Mitigation: deploy UPS backup for power resilience; implement scheduled preventive maintenance; review temperature profiles and chamber status daily; preserve full logs after any outage and consult certification bodies when judging cycle validity. 5.2 Temperature Non-uniformity and Sample-to-sample Variation Poor airflow from overloading, accumulated dust or expired calibration creates uneven thermal distribution. Symptoms include large failure-rate variance across positions in one chamber and inconsistent results across batches. Mitigation: follow sample loading guidelines and preserve airflow channels; regularly clean condensers and air ducts; perform 9-point thermal mapping every 6–12 months to maintain ≤2.0℃ uniformity; mark poor-uniformity zones and avoid placing critical qualification samples there; arrange on-site service for airflow tuning and recalibration when needed. 5.3 Non-compliant Test Reports Auditors frequently reject incomplete reports due to missing ramp rates/dwell times, discontinuous temperature logs, unclear sample serial number traceability, superficial failure analysis or incomplete approval signatures. Mitigation: adopt standardized AEC-Q100 report templates covering all mandatory fields; export native chamber logs to avoid manual transcription errors; maintain sample traceability linking serial numbers, baseline data, runtime logs and post-test results; document full failure analysis for all rejected units; enforce three-level sign-off (test engineer, reviewer, approver). 6. Conclusion AEC-Q100 temperature cycling is a gatekeeper for automotive eMMC, UFS and SSD entering OEM supply chains. The difference between Grade 2 and Grade 1 defines thermal stress intensity, test duration and chamber requirements. Rigorous control across the full test lifecycle — sample preparation, in-test monitoring, post-test characterization and reporting — directly determines qualification success. Lab Companion temperature cycling chambers deliver wide temperature range, precise thermal control, reliable long-run operation and full data traceability, fully supporting AEC-Q100 Grade 1 and Grade 2 qualification for automotive storage. Backed by factory calibration in Dongguan and worldwide after-sales support, Lab Companion provides end-to-end solutions: chamber selection, profile setup and test execution support. We help storage manufacturers complete AEC-Q100 qualification smoothly and gain access to automotive supply chains.
    EN SAVOIR PLUS
  • Three-Level Verification System — Lab Companion Rapid Temperature Change Chamber: AI Compute Hardware Test Architecture
    Sep 09, 2026
    1. Hierarchical Testing Requirements for AI Compute Hardware 1.1 The Validation Gap from Silicon to Full Rack During R&D and mass production of AI compute hardware, a long-standing challenge exists: disconnected temperature validation across test layers. Traditionally, chip vendors perform thermal cycling and temperature testing at die level; board suppliers conduct functional and environmental validation on accelerator cards; server manufacturers run burn-in and stress tests at system level. However, these three tiers often adopt inconsistent standards and disjoint validation logic. Components that pass chip-level testing may suffer temperature-related failures at board level due to improper PCB thermal design. Even fully validated accelerator cards can encounter performance anomalies in full server racks caused by airflow interference and power fluctuation. This validation gap stems directly from the high power density of modern AI hardware. A single AI accelerator chip consumes 300W–700W, with stacked HBM memory creating localized hotspots. One accelerator card with multiple chips and high-capacity HBM reaches 500W–1000W. A complete AI server rack, housing dozens of cards, draws tens of kilowatts. Under such thermal loads, temperature is no longer a standalone environmental parameter, but a systemic variable spanning chips, boards and full racks. A tiered validation framework is required to guarantee thermal reliability at every layer. 1.2 Architecture of the Three-Level Test System Lab Companion establishes a progressive three-level rapid temperature change test system: Chip Level → Board Level → Full Rack Level. Each tier targets distinct specimens, equipment configurations, test profiles and validation priorities, while sharing one core objective: verifying thermal reliability across the entire stack of AI compute hardware. • Chip-level testing: validates thermal cycling tolerance of bare components, assessing packaging, solder joints and HBM stack integrity under rapid temperature transitions. • Board-level testing: evaluates thermal adaptability of accelerator cards, verifying PCB thermal layout, power delivery stability and cooling system performance. • Full rack-level testing: examines system-wide thermal management and multi-device coordination, validating airflow distribution, power allocation and cross-card performance consistency. Test conditions gradually mimic real operational environments. Validation focus evolves from component fatigue resistance to overall system stability, forming a complete thermal verification chain. 2. Chip-Level Rapid Temperature Change Testing 2.1 Test Specimens & Core Objectives Test items include AI accelerators (GPU / ASIC / NPU), HBM high-bandwidth memory, PMIC power management ICs, and high-speed SerDes / Retimer interface chips. These foundational components determine the stability of downstream boards and systems. Key validation goals: 1. Packaging reliability: Detect delamination, cracking and solder fatigue under rapid thermal cycling, with special focus on micro-bump interconnect integrity within HBM stacks. 2. Electrical stability: Monitor timing, power consumption and functional integrity during temperature ramps; verify signal integrity of high-speed interfaces. 3. Post-cycle performance consistency: Check whether computation throughput and power draw drift after repeated thermal cycles. 2.2 Equipment Selection: Small-Chamber High-Precision Models Chip testing involves high sample volumes in compact form factors, demanding tight temperature uniformity and control accuracy. Lab Companion TC series small-volume chambers (34L, 64L, 100L, 180L) are the preferred solution. Compact workspace enables fast thermal stabilization. High-precision variants achieve temperature fluctuation ≤ ±0.3°C and temperature uniformity ≤ ±0.5°C, ensuring hundreds of DUTs experience identical thermal profiles in one cycle. Chips are mounted on dedicated test sockets or burn-in boards secured by custom fixtures. Test cables pass through a port panel fitted with gaskets and thermal insulation to avoid cold leakage and temperature drift, enabling powered real-time monitoring connected to external testers. 2.3 Test Profiles & Parameter Setup Standard chip-level profiles follow JEDEC JESD22-A104 Condition C / G: • Temperature range: -40°C ~ +125°C or -55°C ~ +125°C • Ramp rate: 10°C/min ~15°C/min • Cycle count: 500 ~1000 cycles This profile effectively exposes thermomechanical fatigue in packaging and solder joints. For thermally sensitive devices such as HBM, temperature range and ramp speed can be adjusted per component specifications. Lab Companion TC series covers -70°C ~ +180°C. Five linear ramp rates are selectable: 5 /10 /15 /20 /25°C/min. The programmable touch controller defines multi-segment sequences (heat → high temp soak → cool → low temp soak). The chamber runs automatically and continuously logs temperature curves and alarms for full traceability. 3. Board-Level Rapid Temperature Change Testing 3.1 Test Specimens & Core Objectives Board-level DUTs cover GPU accelerator cards, ASIC inference cards, NPU training cards, AI server motherboards, high-speed switches and storage expansion cards. These populated boards integrate multiple chips, HBM and complex power networks, serving as the functional bridge between components and racks. Key validation goals: 1. PCB thermal design verification: Track temperatures of main die, HBM, PMIC and capacitors; identify hotspots during rapid temperature swings. 2. Power delivery stability: Evaluate output accuracy and dynamic response of multi-rail power supplies (core, HBM, I/O), preventing chip reset or functional failure induced by voltage noise. 3. Cooling system performance: Assess thermal behavior of onboard heatsinks, heat pipes and fans; check thermal throttling at high temperature and fan startup faults at low temperature. 3.2 Equipment Selection: Medium-Volume High-Load Models Accelerator cards are physically large and dissipate significant power when powered on. Lab Companion TC series medium-volume chambers (340L, 600L, 1000L) feature upgraded heating and refrigeration capacity, supporting thermal load ≥100kg aluminum equivalent for one or multiple powered accelerator cards under live workloads. Cards are vertically mounted using custom fixtures to replicate the original server orientation and airflow. External power supplies feed the DUT; PCIe signals are routed via extension cables to external test hosts or local onboard test motherboards. Feedthrough ports are thermally sealed for stable chamber conditions. 3.3 Test Profiles & Parameter Setup Board-level thermal profiles are less aggressive than chip-level stress tests: • Temperature range: -20°C ~ +70°C or 0°C ~ +70°C • Ramp rate: 5°C/min ~10°C/min • Cycle count: 100 ~500 cycles The goal is to validate board-level environmental adaptability rather than stimulate component packaging defects. At high-temperature soak, cards run full compute loads such as matrix operations and model inference to monitor die temperature, HBM temperature, power consumption and throughput. Low-temperature soak validates cold startup reliability. At ramp rates up to 15°C/min, temperature overshoot is controlled ≤ ±0.5°C, ensuring DUTs are not exposed to unintended thermal stress beyond defined limits. 4. Full Rack-Level Rapid Temperature Change Testing 4.1 Test Specimens & Core Objectives Full rack testing covers standalone AI servers, multi-node servers, full AI racks and liquid-cooled servers. This tier most closely replicates real data center deployment and validates system-level thermal management, power distribution and multi-card coordination. Key validation goals: 1. Airflow management: Detect airflow interference, hot air recirculation and concentrated hotspots across multiple servers and accelerator cards. 2. Rack power stability: Validate PDU and power module performance under thermal cycling, avoiding efficiency drop or protective shutdown triggered by temperature. 3. Cross-card performance consistency: Ensure uniform compute performance across all accelerators; prevent rack-wide training degradation caused by thermal throttling of individual cards. 4. Liquid cooling compatibility (if applicable): Verify sealing integrity and heat exchange efficiency of pipes, cold plates and quick-disconnect fittings under thermal cycling. 4.2 Equipment Selection: Large-Volume / Walk-In Custom Systems Standard chambers cannot accommodate full-size server racks with high power draw. Lab Companion TC series supports custom engineering from 80L up to 8000L, including large chambers and walk-in temperature rooms. • 1000L: suitable for single AI server testing • 2000L ~8000L walk-in rooms: designed for full racks or parallel multi-rack testing High-capacity heating/refrigeration offsets heat generated by live servers. Custom air ducts mimic hot aisle / cold aisle airflow of data centers, maintaining consistent inlet air temperature to servers. Reinforced flooring and heavy-duty fixtures support the weight of full server racks. 4.3 Test Profiles & Parameter Setup Full rack profiles simulate moderate temperature fluctuations inside data centers, with milder stress: • Temperature range: 10°C ~ +40°C or 15°C ~ +45°C • Ramp rate: 2°C/min ~5°C/min • Cycle count: 50 ~100 cycles The objective is not to induce component defects, but to evaluate dynamic thermal control response and sustained system stability. During high-temperature soak, full racks run heavy AI training or inference workloads. Monitored metrics include server inlet temperature, CPU/GPU junction temperature, power supply efficiency and total rack power draw. During temperature ramps, engineers track fan speed regulation, liquid cooling flow, temperature control response and performance consistency across all accelerators. Chamber refrigeration and airflow can be fully customized according to rack dimensions and power dissipation to guarantee stable thermal field and realistic air distribution. 5. Lab Companion’s Full-Scale Delivery Capability 5.1 Full Volume Matrix with Unified Standards Lab Companion TC rapid temperature change chambers deliver a complete volume matrix from 34L benchtop units up to 8000L walk-in custom rooms. One brand, consistent precision standards and unified service framework cover chip, board and full rack testing. Customers maintain identical operating workflows and comparable datasets across all three validation tiers, lowering maintenance and training costs. Performance specifications: • Temp fluctuation: ≤ ±0.5°C (high-precision version ≤ ±0.3°C) • Temp uniformity: ≤ ±2.0°C (high-precision version ≤ ±0.5°C) • Linear ramp: 5~25°C/min, optional LN₂ for 30°C/min • Temperature range: -70°C ~ +180°C This portfolio meets requirements ranging from component qualification to data center system simulation. 5.2 Customization & Calibration at Dongguan Manufacturing Base Lab Companion’s R&D and manufacturing center in Dongguan supports mass production of standard chambers plus custom engineering for walk-in systems up to 8000L. Custom options include dedicated card fixtures, high-speed signal feedthrough panels, high-power cable ports and data-center-style airflow designs tailored to AI hardware test requirements. Localized manufacturing shortens lead times compared with imported equipment, matching the fast iteration cycle of AI hardware. Every unit undergoes strict factory validation: ramp rate verification, 9-point temperature mapping, extreme setpoint stability test and long-duration continuous run. Large / walk-in systems additionally complete loaded thermal and airflow validation. Delivery includes full calibration certificates and test reports for lab audit and third-party certification. 5.3 Nationwide Service Network R&D labs and test facilities of AI hardware customers spread across China: Pearl River Delta, Yangtze River Delta, Beijing-Tianjin-Hebei region and western data centers. Lab Companion maintains regional service points for installation, commissioning, periodic calibration and repair. For large walk-in systems, field engineers manage on-site placement, utility connection, airflow tuning and thermal mapping. Annual preventive maintenance covers refrigeration inspection, electrical tightening, temperature calibration and consumable replacement. Remote diagnostics quickly troubleshoot common faults and reduce downtime. 6. Conclusion High power density makes AI compute hardware thermal reliability validation a multi-layer task rather than a single-stage test. Chip-level testing verifies thermomechanical fatigue of packaging and solder joints; board-level testing validates PCB thermal design and power integrity; full rack-level testing confirms system airflow and multi-card performance consistency. These tiers form an end-to-end thermal reliability validation chain. Lab Companion TC rapid temperature change chambers feature wide temperature range, high precision and scalable volume from small benchtop chambers to large walk-in custom rooms. With in-house Dongguan manufacturing and nationwide service support, Lab Companion provides unified thermal test solutions for chip designers, accelerator card vendors and server OEMs. We help customers build standardized, traceable three-level validation workflows and ensure thermal reliability of AI compute hardware through development to mass deployment.
    EN SAVOIR PLUS
  • Lab Companion Thermal Chamber: High-Low Temperature Testing for EV BMS and PV Inverters
    Sep 08, 2026
    1. Real-World Thermal Challenges for New Energy Electronic Components 1.1 Extreme Temperature Cycling in Field Operation New energy vehicles, photovoltaic power generation, and energy storage systems operate in fully exposed outdoor environments, where core electronic units endure drastic temperature swings from extreme cold to extreme heat. Reliability under wide temperature ranges is critical for system safety, efficiency, and service life. A Battery Management System (BMS) is installed inside vehicle battery packs. In cold regions, internal pack temperatures can drop below -20 °C or even -30 °C during winter parking. In summer, solar radiation plus fast-charging heat can raise internal temperatures above 50 °C. The BMS must maintain accurate temperature sampling, cell voltage monitoring, passive/active balancing, and stable communication across the entire operating temperature spectrum. PV inverters and Power Conversion Systems (PCS) face harsher ambient conditions. Desert summer cabinet temperatures can exceed 60 °C, while winter nights drop below -20 °C. Coastal regions combine high temperature with high humidity. Key components including IGBT modules, electrolytic capacitors, magnetic devices, and main control boards are highly temperature-sensitive. Excessive temperature deviation causes derating, over-temperature protection, reduced power generation efficiency, and unexpected system downtime. 1.2 Superimposed Heat Load from High-Power Operation Unlike conventional consumer electronics, new energy power devices generate significant internal heat during high-rate charging, discharging, and full-load operation. Inverters produce continuous high power loss through IGBT switching and conduction, creating steep thermal gradients inside enclosures. When internal heat buildup overlaps with high ambient temperature, component temperatures approach or exceed maximum ratings. For this reason, static temperature storage testing is insufficient. Real-world reliability verification requires dynamic, powered testing under temperature cycling. Chambers must support full-load operation, long-duration thermal stability, and real-time data monitoring to validate thermal derating, protection logic, and operational stability. 2. Standardized High/Low Temperature Test Items for BMS and Inverters 2.1 BMS Testing: Full-Range Temperature Accuracy & Control Stability BMS temperature testing focuses on data accuracy, cold-start reliability, and thermal balancing performance across extreme conditions. Low-temperature startup test: Soak at -20 °C to -40 °C before power-on to verify initialization, cell voltage and temperature sampling accuracy, and CAN communication stability under freezing conditions. High-temperature operational test: Continuous running at +60 °C to +85 °C under fast-charging and high-discharge load conditions. Engineers monitor temperature sampling error, over-temperature protection thresholds, and balancing current stability. Temperature accuracy is fundamental for SOC estimation, charge/discharge cutoff control, and fault protection. Minor sampling deviations may lead to incorrect battery strategy and potential safety risks. Lab Companion chambers support precise point-to-point calibration across -40 °C to +85 °C to validate BMS algorithm robustness. 2.2 PV Inverter & PCS Testing: Full-Load Stability & Thermal Derating Verification Inverter testing emphasizes full-load operational reliability and temperature-based derating characteristics under extreme ambient conditions. High-temperature full-load test: Operate at rated DC input and full AC output for minimum 4 hours at +40 °C to +60 °C. Monitor IGBT junction temperature, capacitor temperature, control board temperature, system efficiency, THD, voltage/frequency stability, and over-temperature protection behavior. Validated results ensure no unexpected derating or shutdown within specified temperature limits. Low-temperature performance test: Verify cold-start capability and low-load stability at -20 °C to -40 °C. Low temperatures cause capacitance drop and ESR increase in electrolytic capacitors, which may induce bus voltage fluctuation. Tests confirm reliable startup, normal grid-tie/off-grid switching, and no false alarms in cold environments. 2.3 Global Compliance Standards All test procedures comply with internationally recognized standards, including IEC 60068-2-1 / IEC 60068-2-2, GB/T 2423, as well as industry-specific specifications for BMS (QC/T 897, GB/T 31467) and inverters (NB/T 32004, GB/T 37408, GB/T 34120). 3. Lab Companion Chamber Technical Advantages for New Energy Testing 3.1 Full Volume Range for High-Power Device Testing Lab Companion thermal chambers cover a full volume range from 34 L to 1500 L, fully matching new energy testing requirements. Medium and large chambers (340 L–1500 L) are specially optimized for high-calorific and heavy-load samples such as BMS units, onboard controllers, PV inverters, and energy storage PCS systems. Enhanced heating and cooling systems guarantee rapid temperature recovery and uniform thermal field even with high-power heat-generating DUTs. SUS304 stainless steel interior provides corrosion resistance against electrolyte vapor and industrial dust. Customizable shelf spacing and load-bearing structures ensure stable sample placement and unobstructed internal airflow. 3.2 Ultra-Wide Temperature Range & High Precision Stability Lab Companion chambers feature a wide temperature range of -70 °C to +150 °C, with customizable low-temperature thresholds to match different project specifications. The operational range fully covers standard BMS and inverter test boundaries with sufficient safety margin for long-term stable operation. Precision performance meets strict industrial testing requirements: Temperature fluctuation ≤ ±0.5 °C, temperature uniformity ≤ ±2.0 °C (high-precision version ≤ ±0.3 °C). Equipped with proprietary Q8 intelligent control system and balanced temperature & humidity control (BTHC) technology, the chamber avoids temperature overshoot and oscillation, delivering consistent, repeatable thermal conditions for accurate algorithm calibration and reliability validation. 3.3 Customized Cable Ports for Powered & Live Testing All Lab Companion environmental chambers support customized insulated cable ports for power cables, CAN/RS485 communication lines, and sensor wiring. The sealed and insulated port design prevents cold leakage and thermal field disturbance during long-duration powered tests. Customers can perform real-time data acquisition including BMS cell voltage, temperature sampling error, SOC balance status, and fault logs. For inverters, users can connect external DC power sources and AC load banks to conduct full-load continuous aging and thermal derating testing, with complete data logging and export functions for technical reports and certification documents. 4. Global Service & Technical Support Model 4.1 Factory Direct Customization & Global Delivery Lab Companion is a national high-tech enterprise and specialized & sophisticated manufacturer based in Dongguan, China. With 21 years of experience in environmental test equipment R&D and manufacturing, the brand holds Madrid International Trademark registration, as well as EU, UK, and Germany trademark certifications, supporting global project qualification and customer recognition. We provide worldwide direct shipping and factory customization services, including customized internal dimensions, high-power port configurations, special load-bearing shelves, and tailored thermal solutions for customer-specific inverter and BMS test standards. 4.2 Global Online Remote Technical Support To serve global customers efficiently, Lab Companion adopts an overseas online support system. We do not provide local after-sales service teams in foreign countries, but deliver full-life-cycle remote technical support. Our professional international support team providesonline installation guidance, operation training, parameter calibration, program debugging, and remote fault diagnosis. Most technical issues can be resolved efficiently via online guidance, eliminating regional service barriers and ensuring stable and continuous equipment operation for global laboratories and factories. 4.4 Global Industry Application Cases Lab Companion thermal test chambers are widely used in global new energy vehicle, photovoltaic, and energy storage industries. Our equipment has been adopted by automotive electronics suppliers, renewable energy manufacturers, and university research institutions for BMS temperature calibration, inverter high-low temperature cycling, full-load aging, and thermal derating validation. Stable temperature accuracy and reliable long-duration operation help customers optimize product algorithms, improve extreme environmental adaptability, and accelerate product certification and mass production. 5. Conclusion Extreme temperature adaptability is a core indicator of reliability for EV BMS, PV inverters, and energy storage converters. Professional high-low temperature testing is essential for product R&D, performance optimization, and global market certification. Lab Companion environmental test chambers provide ultra-wide temperature range, high-precision thermal stability, high-load compatibility, and customizable powered test interfaces, perfectly matching the full-cycle reliability testing needs of new energy power electronic products. Supported by factory direct customization and professional global remote technical support, we deliver stable, cost-effective, and standardized thermal testing solutions for global new energy enterprises, helping customers enhance product durability and market competitiveness in all-climate operating scenarios.
    EN SAVOIR PLUS
  • Lab Companion Thermal Cycling Test Chambers: Application Practice for Optical Modules and Passive Optical Components Lab Companion Thermal Cycling Test Chambers: Application Practice for Optical Modules and Passive Optical Components
    Sep 07, 2026
    1. Core Challenges: Temperature Sensitivity of Optical Communication Components 1.1 Optical Parameter Drift Caused by Temperature Change Optical communication components are far more temperature-sensitive than conventional electronic devices. Temperature fluctuation directly shifts key optical parameters and degrades system transmission performance. For active optical modules, DFB laser wavelength drifts approximately 0.1 nm per °C. When temperature rises from 0 °C to 70 °C, the total wavelength shift can exceed 7 nm. Once the drift exceeds the channel spacing of WDM systems, crosstalk and bit error rate will increase significantly. Meanwhile, temperature variation changes laser threshold current, output optical power and extinction ratio, causing unstable emission performance at extreme temperatures. Passive optical devices also suffer from severe temperature-dependent drift. AWG devices based on PLC technology feature a high thermo-optic coefficient of 1.8×10⁻⁴/°C. Temperature change alters the effective refractive index of waveguides and shifts the central wavelength. Uncompensated AWG modules can drift several nanometers across −40 °C to +85 °C. In addition, temperature fluctuation changes insertion loss of optical splitters and return loss of fiber connectors. Therefore, full-range thermal cycling testing is essential to verify stable optical performance. 1.2 Packaging Reliability Risks Under Thermal Cycling Repeated temperature changes generate thermo-mechanical stress inside optical components. An optical module consists of multiple materials including laser chips, detectors, lenses, isolators, ceramics, metal shells and PCB substrates. Different thermal expansion coefficients create shear stress at bonding and soldering interfaces during temperature cycling. Long-term thermal cycling may lead to optical misalignment, bonding failure or solder crack issues. For fiber-coupled devices, submicron alignment precision is extremely sensitive to tiny structural deformation. Even minor displacement can reduce coupling efficiency. For this reason, continuous thermal cycling testing is a mandatory reliability procedure for optical components before mass production. 2. Global Standards and Test Specifications for Optical Thermal Cycling 2.1 International Standard Framework Telcordia GR-468-CORE serves as the primary guideline for optical component reliability testing. It defines thermal cycling as a critical qualification item. Standard test conditions cover −40 °C to +85 °C with a minimum of 500 cycles for commercial products. For high-reliability scenarios such as outdoor base stations and industrial equipment, 1000 cycles are required. Tests also comply with IEC 60068-2-14 Nc temperature variation standards. For high-speed data center optical modules, design and reliability requirements follow SFF-8431 and SFF-8432 MSA specifications. All optical and electrical parameters must remain within acceptable tolerance after long-cycle temperature shocks. 2.2 Standard Test Profiles and Operation Requirements The industry-standard temperature range is −40 °C to +85 °C, extended to −40 °C to +105 °C for industrial-grade products. A complete cycle includes four stages: low-temperature soaking, linear heating, high-temperature soaking, and linear cooling. Soaking time at extreme temperatures is no less than 15 minutes to ensure full temperature stabilization inside components. Typical ramp rate ranges from 5 °C/min to 15 °C/min. Long-duration testing requires continuous and stable equipment operation. 500 cycles take approximately 40 days of non-stop running, while 1000 cycles take up to 80 days. Any temperature instability or system interruption will invalidate test data. Stable chamber performance is critical for mass qualification. 2.3 In-Situ Optical Parameter Monitoring Different from general electronic testing, optical component qualification requires real-time optical parameter monitoring during temperature cycling. Active modules require continuous monitoring of optical power, extinction ratio, eye diagram quality, receiver sensitivity and operating current. Passive devices require testing of insertion loss, return loss, wavelength shift and PDL. Real-time measurement requires external connection to optical power meters, spectrum analyzers and BER testers through fiber feedthrough ports. The feedthrough design must ensure effective sealing and thermal insulation to avoid cold leakage, internal frosting and temperature fluctuation. Lab Companion provides customizable multi-channel fiber feedthrough panels to support stable long-cycle optical monitoring. 3. Lab Companion Thermal Cycling Chamber: Optimized for Optical Industry Testing 3.1 Ultra-Wide Temperature Range and High Precision Stability Lab Companion thermal cycling chambers cover a temperature range from −70 °C to +150 °C, fully exceeding GR-468 standard requirements. The wide temperature margin ensures stable operation even during months of continuous cycling, without running at extreme load limits. The chamber achieves temperature fluctuation ≤ ±0.5 °C and temperature uniformity ≤ 2.0 °C, delivering far higher stability than standard requirements. The optimized air duct circulation system ensures uniform temperature distribution across the entire workspace. It eliminates data deviation caused by local temperature difference and guarantees accurate, repeatable optical performance evaluation. 3.2 Adjustable Ramp Rates and Dual Operation Modes Lab Companion equipment supports five adjustable ramp rates: 5 °C/min, 10 °C/min, 15 °C/min, 20 °C/min and 25 °C/min. Both linear and non-linear temperature profiles are available. Linear mode strictly follows IEC and GR-468 standard curves for official certification and cross-lab data comparison. Non-linear mode simulates real-world environmental temperature changes for accelerated reliability verification in R&D stages. For high-stress screening, optional liquid nitrogen auxiliary cooling increases the maximum cooling rate to 30 °C/min, greatly improving mass testing efficiency. 3.3 Multi-Size Chamber and Customized Fixture Solutions Optical components feature small size and large batch testing demands. Lab Companion provides multiple chamber volumes: 80 L, 150 L and 225 L for R&D and small-batch qualification; 340 L and 600 L models for high-volume mass production screening. Multi-layer racks support simultaneous testing of hundreds of optical modules and passive components. Customized fixtures are available for optical-specific applications. SFP/QSFP module test brackets support independent power supply and high-speed signal connection for real-time BER testing. Dedicated fiber management trays protect AWG and splitter fibers from excessive bending stress. SUS304 stainless steel inner chamber ensures high cleanliness and long-term durability. 4. Localized Manufacturing and Global Service Support 4.1 Customized Manufacturing and Fast Delivery Founded in 2005, Lab Companion (Guangdong Hongzhan Technology) is a national high-tech enterprise and specialized & sophisticated manufacturer based in Dongguan, China. It is strategically located near the optical communication industrial clusters of Shenzhen and Guangzhou, enabling fast customized solutions and short lead-time delivery. All chambers undergo strict factory calibration, including 9-point temperature uniformity testing, ramp rate verification and long-cycle stability validation. Before delivery, optical test-oriented optimization and feedthrough sealing performance testing ensure full compliance with customer qualification standards. 4.2 Global Service Network for Long-Term Stable Operation Optical reliability tests require weeks or months of non-stop operation. Equipment stability and rapid after-sales support are essential. Lab Companion operates 16 service centers across China and overseas support networks, providing fast response, on-site debugging, calibration and maintenance services. Remote diagnosis functions quickly identify temperature control errors and sensor faults. Annual maintenance programs include refrigeration system inspection, electrical tightening, temperature field recalibration and wearing part replacement, ensuring long-term precision and stability during continuous cycling tests. 4.3 Verified Field Application Results Lab Companion thermal cycling chambers are widely adopted by optical module manufacturers, passive component suppliers and communication equipment enterprises. The equipment stably supports more than 500 consecutive thermal cycles with consistent temperature accuracy and reliable ramp rate control. The sealed fiber feedthrough design effectively prevents cold leakage and internal frosting during long-term optical monitoring. Custom fixtures ensure standardized sample placement and safe fiber routing. Customers obtain complete full-temperature optical performance curves to optimize temperature compensation algorithms and packaging structures, improving product reliability for 5G, data center and outdoor communication applications. 5. Conclusion Thermal cycling testing is an indispensable procedure for optical component reliability qualification. It effectively exposes wavelength drift, power attenuation, insertion loss variation and packaging structural risks under alternating temperature conditions, fully meeting GR-468, IEC and GB/T standard requirements. Lab Companion thermal cycling test chambers provide ultra-wide temperature range, high-precision temperature control, multi-speed ramp adjustment and professional optical test customization capabilities. The dedicated fiber feedthrough structure and customized fixture system solve the core difficulties of real-time optical monitoring during dynamic temperature cycling. Backed by 21 years of professional R&D and manufacturing experience, localized customization capability and global after-sales service network, Lab Companion delivers one-stop test solutions for optical communication customers. It helps enterprises build standardized and traceable reliability test systems, ensuring stable and durable performance of optical modules and passive components in global 5G and data center infrastructure applications.
    EN SAVOIR PLUS
  • Lab Companion Temperature Test Chambers: Full-Lifecycle SSD Testing Solutions from R&D to Mass Production Screening
    Sep 04, 2026
    1. SSD Reliability Testing: More Than Basic Temperature Simulation Solid-state drives (SSDs) undergo rigorous environmental reliability validation throughout their entire journey from prototype design to mass delivery. Every development stage demands distinct testing standards: performance boundary verification in R&D, standard compliance validation in design verification, process stability evaluation during pilot production, and early failure screening in mass manufacturing. Each phase requires different equipment capabilities. R&D requires ultra-wide temperature range and high-precision control to capture accurate limit performance data. Design verification prioritizes test repeatability and consistency. Pilot production needs scalable batch testing capacity. Mass production demands high throughput, automated operation, and long-term stable runtime performance. A single versatile test chamber that covers the full development lifecycle greatly improves testing efficiency and reduces equipment investment costs. Established in 2005, Lab Companion is a national high-tech enterprise and specialized & sophisticated manufacturer based in Dongguan, China. With 20+ years of focus on environmental reliability test equipment, our PS series temperature and humidity chambers and TC series rapid thermal cycling chambers serve as one-stop testing platforms for consumer and enterprise-grade SSD full-lifecycle validation. 2. R&D Phase: Performance Boundary Exploration Under Extreme Conditions During SSD prototype development, engineers must verify the operational stability of main controllers, NAND flash particles, and complete drives across diverse temperature environments. Small-batch engineering samples require wide-spectrum temperature testing with strict precision requirements. Lab Companion PS series thermal test chambers feature a broad temperature range of-70℃ to +150℃. This fully covers consumer SSD testing scenarios from -10℃ cold startup to +70℃ high-temperature continuous read-write operation. It also meets enterprise SSD thermal cycling standards (40℃ to 85℃) and reserves sufficient margin for vehicle-grade SSD extreme validation (-40℃ to 125℃). The chamber delivers industry-leading precision: temperature fluctuation ≤±0.5℃, temperature deviation ≤±2.0℃, and temperature uniformity ≤±2.0℃. Compliant with the GB/T 10592-2023 international equipment standard, it ensures uniform environmental stress across all sample positions and highly repeatable test results. For advanced R&D validation, Lab Companion chambers support docking with Advantest and Teradyne IC test systems to verify core chip functionality under extreme temperatures. External T/K-type thermocouples accurately monitor real sample surface temperatures, ensuring precise thermal soak validation. 3. DVT Phase: Standard Compliance and Repeatable Validation In the Design Verification Test (DVT) stage, SSD products must comply with global JEDEC industry standards, includingJESD218 and JESD22-A104. Consumer SSDs undergo 25℃ to 70℃ thermal cycling to simulate daily usage and verify stability and data integrity. Enterprise SSDs require 40℃ to 85℃ cycling with 100% random read-write load to validate QoS latency consistency under high-load operation. DVT testing requires outstanding equipment repeatability to eliminate environmental errors from batch-to-batch results. Lab Companion’s stable temperature control ensures identical test conditions for every cycle. The programmable controller stores multiple custom test profiles for automatic cyclic operation, minimizing human-induced variables. For long-duration durability tests requiring hundreds or thousands of thermal cycles, Lab Companion chambers support 1000+ hours of continuous stable operation. Built-in UPS power backup and breakpoint resume functions automatically restore testing after unexpected power outages, preventing sample damage and data loss. 4. PVT Phase: Mass Production Process Stability Verification During Pilot Verification Test (PVT), manufacturers validate mass-production process consistency via medium-batch sample testing. Reliable batch thermal cycling results are critical for confirming production yield stability. Lab Companion chambers adopt a flexible multi-layer tray structure adaptable to various SSD dimensions. Standard volume options range from 80L to 1000L, with custom capacities from 80L to 8000L available to suit lab-scale R&D and medium-volume pilot testing. Each SSD sample supports independent power supply and individual data monitoring. The system automatically records full-test data including temperature curves, ramp rates, and dwell time, and generates standardized pass/fail test reports. All data can be integrated into factory quality traceability systems to support mass production validation decisions. 5. Mass Production Phase: High-Efficiency Stress Screening and Early Failure Elimination High-volume SSD mass production requires fast, cost-effective reliability screening to eliminate early failed units without compromising throughput. Lab Companion ESS Environmental Stress Screening Chambers are purpose-built for production-line accelerated testing. The ESS series provides adjustable thermal ramp rates of 5℃/min to 15℃/min within -55℃ to +85℃, with temperature uniformity ≤2℃. Pre-configured standard test profiles allow one-click switching between consumer and enterprise SSD screening procedures. The multi-layer tray design enables high-density simultaneous testing of hundreds of SSDs. Equipped with independent power and data acquisition channels, the system supports 24/7 unattended automated operation, significantly improving production-line testing efficiency. In practical industrial applications, a Tier 1 automotive supplier reduced SSD early failure rate from 800ppm to below 200ppm after deploying the Lab Companion TC-408 rapid thermal cycling chamber (10℃/min ramp rate), demonstrating reliable mass-screening performance. 6. Full-Cycle Safety Protection and Complete Data Traceability High-value SSD prototypes and mass-production components require rigorous safety protection and full data traceability throughout testing. Lab Companion chambers adopt multi-level safety mechanisms: independent mechanical over-temperature protection (hardware-level cutoff unaffected by software failures), compressor over-pressure/overload/delay startup protection, dual over-temperature protection for heating systems, and comprehensive electrical protection against phase loss, leakage, and grounding faults. These designs fully protect test samples from damage. For quality management, the system supports batch code scanning and full-process data archiving. All temperature curves, test parameters, and operation logs are permanently traceable. Intelligent fault diagnosis displays error codes and troubleshooting steps directly on the screen, with remote alarm notifications available via mobile and PC terminals for unattended operation security. 7. Conclusion Reliability temperature testing runs through the entire SSD lifecycle: R&D boundary exploration, DVT standard compliance verification, PVT process validation, and mass production failure screening. With -70℃ to +150℃ ultra-wide temperature range, ±0.5℃ precise temperature control, excellent temperature uniformity, and scalable batch testing capability, Lab Companion PS and TC series chambers deliver a fully compatible solution for SSD industry from laboratory R&D to factory mass production. Serving over 3000 global manufacturers, research institutions and testing labs, Lab Companion has proven its capability as a reliable full-lifecycle testing partner for semiconductor storage reliability validation.
    EN SAVOIR PLUS
  • Lab Companion MES/EAP-Enabled Temperature Test Chambers: Quantifiable Improvements in Efficiency, Cost, Quality and Factory Management
    Sep 03, 2026
    1. Overview: Turning Reliability Testing from “Cost Center” into “Data Asset” In semiconductor, automotive electronics, new energy and optical communication manufacturing, environmental reliability testing has long been treated as a necessary cost. Traditional temperature chambers operate as standalone devices. Test data is stored locally, isolated from factory systems, and requires heavy manual work to organize and verify. Lab Companion network-enabled temperature and thermal cycling chambers solve this industry pain point. By supporting MES and EAP system integration, our testing equipment becomes a connected node on the smart production line. All test data is digitized, traceable and automatically synchronized to factory management systems. The upgrade delivers clear, quantifiable improvements in productivity, operational cost, quality compliance and factory transparency. 2. Efficiency Gains: Automate Manual Workflows Most testing bottlenecks are not caused by device performance, but by repetitive manual operations: recipe setup, batch entry, data logging and report generation. Lab Companion smart chambers eliminate these inefficient workflows. 2.1 One-click standard test recipes Equipped with an industrial H-Touch controller, the chamber supports up to 1200 programmable cycling segments. Industry-standard test profiles including JESD22-A104, JESD22-A106B and AEC-Q100 are preloaded and available for one-click activation. Manufacturers no longer need manual parameter configuration during product changeover. It eliminates human setup errors, avoids invalid testing and shortens setup time significantly. 2.2 Auto batch logging and PDF report output The device supports barcode batch scanning for automatic product binding. Once a test completes, the system automatically generates a standardized PDF report containing temperature curves, ramp rates, dwell time and pass/fail results. All data is uploaded directly to MES. This replaces manual report sorting, which traditionally takes around 40 minutes per batch, saving substantial labor hours for mass production. 2.3 Local real-time data recording and direct USB export Real-time test curves are automatically saved locally. Operators can export complete historical data via USB without extra host software. Data retrieval and technical review become fast and convenient. 3. Cost Reduction: Lower Energy Consumption & Maintenance Cost For 24/7 continuous environmental screening, energy consumption and equipment maintenance are the two largest operational costs. Lab Companion optimizes both through intelligent control and upgraded hardware. 3.1 AI energy-saving control, 28%–38% power reduction Traditional on-off compressors waste massive energy during stable temperature holding. Lab Companion chambers adopt variable-frequency compressors + electronic expansion valves, paired with self-developed Q8 intelligent control algorithm. The system dynamically adjusts compressor frequency, heating output and airflow based on real-time load and ambient conditions. Temperature overshoot is controlled below 0.8%. Compared with conventional chambers, overall energy consumption drops by 28%–38%, and steady-state power saving exceeds 40%. 3.2 AI predictive fault diagnosis, 70% fewer failures Traditional maintenance is passive and reactive. Lab Companion’s real-time component monitoring system predicts potential failures in advance. Data shows the intelligent warning system reduces equipment failure rate by 70% and cuts maintenance costs by 30%. The built-in 600,000 offline data storage points ensure zero data loss during network disconnection. Data will be auto-resynchronized once the network recovers, preventing rework caused by missing records. 4. Quality Upgrade: Full Lifecycle Traceability & Compliance For high-precision industries, reliable, auditable and reproducible test data is the core of quality certification and supply-chain compliance. 4.1 Complete data chain from batch to final judgment Via OPC UA and Modbus TCP protocols, the chamber synchronizes all test parameters to MES in real time, including temperature profiles, cycling speed, holding duration and pass/fail status. It builds a full traceability chain: Batch — Device — Recipe — Curve — Test Result. 4.2 No manual filling for audit and certification All data is automatically archived with unified standards. No manual spreadsheet adjustment is required before customer audits or industry certification reviews. It greatly reduces compliance risks and preparation workload. 4.3 Stable data recording for long-duration tests With 600,000 offline storage records, the system supports ultra-long aging and cycling tests for optical components and new energy cells. Continuous data integrity is guaranteed even under unstable network conditions. 5. Smart Factory Management: Transparent & Remote Operation Standalone test chambers create “black boxes” on production lines. Lab Companion networking transforms discrete testing equipment into visible, manageable production assets. 5.1 Real-time test progress visualization MES management terminals can monitor real-time status of all connected chambers, including running recipes, test progress and completion results. Production supervisors can schedule tasks accurately and optimize equipment utilization. 5.2 Full remote monitoring & control Based on web-based Q8 control system, engineers can remotely view temperature curves, adjust parameters, start/stop tests and check historical records via PC or mobile devices. On-site attendance is no longer mandatory, which greatly improves management efficiency for multi-site factories. 5.3 Instant alarm for abnormal status System errors and parameter deviations trigger real-time alerts. Maintenance teams can respond rapidly to minimize downtime and ensure continuous production screening. 6. Core Specifications of Lab Companion Networked Test Chambers • Product Series: TC/ESS Rapid Temperature Change Chamber, TS/PS Temperature & Humidity Chamber, OVEN High-Temperature Aging Chamber • Temperature Range: -70℃ ~ +150℃; max +300℃ for high-temp models • Temperature Accuracy: Fluctuation ±0.5℃, Deviation ±2.0℃, Uniformity ≤2.0℃ • Temperature Ramp Rate: 5℃/min ~ 25℃/min optional • Capacity Range: 80L ~ 2000L full coverage • Standard Interface: RS485, Ethernet • Industrial Protocols: OPC UA / Modbus TCP optional; SECS/GEM customizable for semiconductor FAB EAP integration • Smart Functions: 1200-step programmable recipes, 600,000 offline data storage, AI predictive maintenance, remote control 7. Conclusion: Measurable Benefits for Smart Manufacturing Lab Companion MES/EAP-enabled environmental test chambers deliver fully verified, data-driven upgrades for modern factories: • Higher Efficiency: Automated recipes, auto-reporting and barcode tracing eliminate repetitive manual work and human errors. • Lower OPEX: 28%–38% energy saving and 30% less maintenance cost bring long-term operational benefits. • Reliable Quality: Full-process traceable data meets global automotive, semiconductor and new energy certification standards. • Digital Management: Transparent, remote and intelligent operation fits Industry 4.0 smart factory requirements. Proven in semiconductor, automotive electronics, optical communication and new energy production lines, Lab Companion networked testing solutions help global manufacturers turn reliability testing from a pure cost center into a valuable, data-driven quality control asset.
    EN SAVOIR PLUS
  • Lab Companion MES/EAP-Enabled Temperature Test Chambers: Quantifiable Improvements in Efficiency, Cost, Quality and Factory Management Lab Companion MES/EAP-Enabled Temperature Test Chambers: Quantifiable Improvements in Efficiency, Cost, Quality and Factory Management
    Sep 02, 2026
    1. Overview: Turning Reliability Testing from “Cost Center” into “Data Asset” In semiconductor, automotive electronics, new energy and optical communication manufacturing, environmental reliability testing has long been treated as a necessary cost. Traditional temperature chambers operate as standalone devices. Test data is stored locally, isolated from factory systems, and requires heavy manual work to organize and verify. Lab Companion network-enabled temperature and thermal cycling chambers solve this industry pain point. By supporting MES and EAP system integration, our testing equipment becomes a connected node on the smart production line. All test data is digitized, traceable and automatically synchronized to factory management systems. The upgrade delivers clear, quantifiable improvements in productivity, operational cost, quality compliance and factory transparency. 2. Efficiency Gains: Automate Manual Workflows Most testing bottlenecks are not caused by device performance, but by repetitive manual operations: recipe setup, batch entry, data logging and report generation. Lab Companion smart chambers eliminate these inefficient workflows. 2.1 One-click standard test recipes Equipped with an industrial H-Touch controller, the chamber supports up to 1200 programmable cycling segments. Industry-standard test profiles including JESD22-A104, JESD22-A106B and AEC-Q100 are preloaded and available for one-click activation. Manufacturers no longer need manual parameter configuration during product changeover. It eliminates human setup errors, avoids invalid testing and shortens setup time significantly. 2.2 Auto batch logging and PDF report output The device supports barcode batch scanning for automatic product binding. Once a test completes, the system automatically generates a standardized PDF report containing temperature curves, ramp rates, dwell time and pass/fail results. All data is uploaded directly to MES. This replaces manual report sorting, which traditionally takes around 40 minutes per batch, saving substantial labor hours for mass production. 2.3 Local real-time data recording and direct USB export Real-time test curves are automatically saved locally. Operators can export complete historical data via USB without extra host software. Data retrieval and technical review become fast and convenient. 3. Cost Reduction: Lower Energy Consumption & Maintenance Cost For 24/7 continuous environmental screening, energy consumption and equipment maintenance are the two largest operational costs. Lab Companion optimizes both through intelligent control and upgraded hardware. 3.1 AI energy-saving control, 28%–38% power reduction Traditional on-off compressors waste massive energy during stable temperature holding. Lab Companion chambers adopt variable-frequency compressors + electronic expansion valves, paired with self-developed Q8 intelligent control algorithm. The system dynamically adjusts compressor frequency, heating output and airflow based on real-time load and ambient conditions. Temperature overshoot is controlled below 0.8%. Compared with conventional chambers, overall energy consumption drops by 28%–38%, and steady-state power saving exceeds 40%. 3.2 AI predictive fault diagnosis, 70% fewer failures Traditional maintenance is passive and reactive. Lab Companion’s real-time component monitoring system predicts potential failures in advance. Data shows the intelligent warning system reduces equipment failure rate by 70% and cuts maintenance costs by 30%. The built-in 600,000 offline data storage points ensure zero data loss during network disconnection. Data will be auto-resynchronized once the network recovers, preventing rework caused by missing records. 4. Quality Upgrade: Full Lifecycle Traceability & Compliance For high-precision industries, reliable, auditable and reproducible test data is the core of quality certification and supply-chain compliance. 4.1 Complete data chain from batch to final judgment Via OPC UA and Modbus TCP protocols, the chamber synchronizes all test parameters to MES in real time, including temperature profiles, cycling speed, holding duration and pass/fail status. It builds a full traceability chain: Batch — Device — Recipe — Curve — Test Result. 4.2 No manual filling for audit and certification All data is automatically archived with unified standards. No manual spreadsheet adjustment is required before customer audits or industry certification reviews. It greatly reduces compliance risks and preparation workload. 4.3 Stable data recording for long-duration tests With 600,000 offline storage records, the system supports ultra-long aging and cycling tests for optical components and new energy cells. Continuous data integrity is guaranteed even under unstable network conditions. 5. Smart Factory Management: Transparent & Remote Operation Standalone test chambers create “black boxes” on production lines. Lab Companion networking transforms discrete testing equipment into visible, manageable production assets. 5.1 Real-time test progress visualization MES management terminals can monitor real-time status of all connected chambers, including running recipes, test progress and completion results. Production supervisors can schedule tasks accurately and optimize equipment utilization. 5.2 Full remote monitoring & control Based on web-based Q8 control system, engineers can remotely view temperature curves, adjust parameters, start/stop tests and check historical records via PC or mobile devices. On-site attendance is no longer mandatory, which greatly improves management efficiency for multi-site factories. 5.3 Instant alarm for abnormal status System errors and parameter deviations trigger real-time alerts. Maintenance teams can respond rapidly to minimize downtime and ensure continuous production screening. 6. Core Specifications of Lab Companion Networked Test Chambers • Product Series: TC/ESS Rapid Temperature Change Chamber, TS/PS Temperature & Humidity Chamber, OVEN High-Temperature Aging Chamber • Temperature Range: -70℃ ~ +150℃; max +300℃ for high-temp models • Temperature Accuracy: Fluctuation ±0.5℃, Deviation ±2.0℃, Uniformity ≤2.0℃ • Temperature Ramp Rate: 5℃/min ~ 25℃/min optional • Capacity Range: 80L ~ 2000L full coverage • Standard Interface: RS485, Ethernet • Industrial Protocols: OPC UA / Modbus TCP optional; SECS/GEM customizable for semiconductor FAB EAP integration • Smart Functions: 1200-step programmable recipes, 600,000 offline data storage, AI predictive maintenance, remote control 7. Conclusion: Measurable Benefits for Smart Manufacturing Lab Companion MES/EAP-enabled environmental test chambers deliver fully verified, data-driven upgrades for modern factories: • Higher Efficiency: Automated recipes, auto-reporting and barcode tracing eliminate repetitive manual work and human errors. • Lower OPEX: 28%–38% energy saving and 30% less maintenance cost bring long-term operational benefits. • Reliable Quality: Full-process traceable data meets global automotive, semiconductor and new energy certification standards. • Digital Management: Transparent, remote and intelligent operation fits Industry 4.0 smart factory requirements. Proven in semiconductor, automotive electronics, optical communication and new energy production lines, Lab Companion networked testing solutions help global manufacturers turn reliability testing from a pure cost center into a valuable, data-driven quality control asset.
    EN SAVOIR PLUS
1 2 3 4 5 6 7
Un total de 7pages

laisser un message

laisser un message
Si vous êtes intéressé par nos produits et souhaitez en savoir plus, veuillez laisser un message ici, nous vous répondrons dès que possible.
soumettre

Maison

Des produits

WhatsApp

Contactez-nous